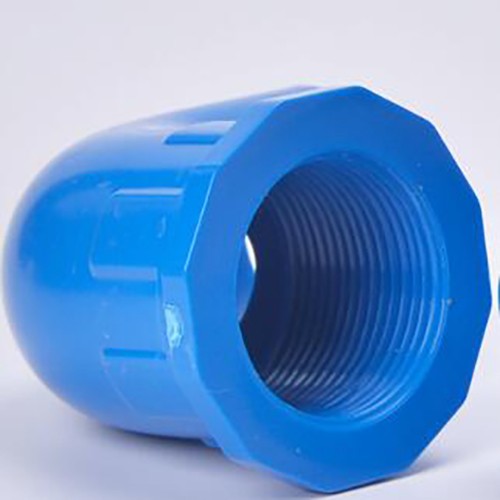
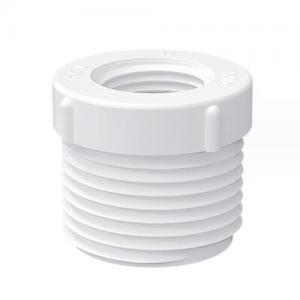
Food Grade PP Thread Pipe Fitting (Multi-Cavities) / Plastic Threaded Caps & Plugs
Processing Capabilities for Plastic Threaded Caps & Plugs
| Item | Detailed Capabilities |
|---|---|
| Material (Housing) | PVC, CPVC, PP, Nylon (PA6/PA66), PVDF, ABS, PE, or custom engineering plastics |
| UV Stability | UV-stabilized options available for outdoor applications (PVC, CPVC, PP) |
| Shape / Style | Hexagonal head, round head with knurling, countersunk head, flanged cap, ribbed cap, tapered plug |
| Connection Type | Female Threaded (to cap male fittings), Male Threaded (plug), Smooth (for masking) |
| Port Size | 1/8" to 6" (DN6–DN150), custom sizes available |
| Thread Standard | BSP (G), NPT, Metric (M), UNF, or custom thread profiles |
| Pressure Rating | 0.6–1.6 MPa (6–16 bar), depending on material and design (Low pressure for protective caps) |
| Operating Temperature | -20°C to 95°C (depending on material: PVC 0–60°C, CPVC 0–95°C, PP 0–90°C, Nylon -40–120°C) |
| Sealing Method | Thread sealant (PTFE tape), O-ring, gasket, or flat gasket inside the cap |
| Surface Finish | Smooth, textured, matte, or glossy finishes available |
| Color | Blue, Grey, white, black, red, yellow, or custom colors matched to customer requirements |
| Processing Tolerance | Thread tolerance ±0.1mm, Diameter tolerance ±0.1mm, Length tolerance ±0.5mm |
| Certifications | ISO9001, ROHS, CE, NSF, food-grade options available |
| Applications | Thread protection during shipping, masking during painting/coating, plumbing, irrigation, chemical processing, HVAC, marine, aquarium, and industrial fluid handling |
| Mold Cavitation | 1x16 (16 cavities per mold) – Standard for high-volume production |
Injection Molding Process for Plastic Threaded Caps (Multi-Cavities Mold)
1. Raw Material Preparation
Select high-quality PVC, CPVC, PP, Nylon (PA6/PA66), or PVDF pellets based on application requirements (pressure, temperature, chemical compatibility). The raw material is dried (for Nylon and PP) and pre-conditioned to remove moisture, ensuring optimal molding performance and preventing surface defects like silver streaks or bubbles.
2. Injection Molding (1x16 Multi-Cavity)
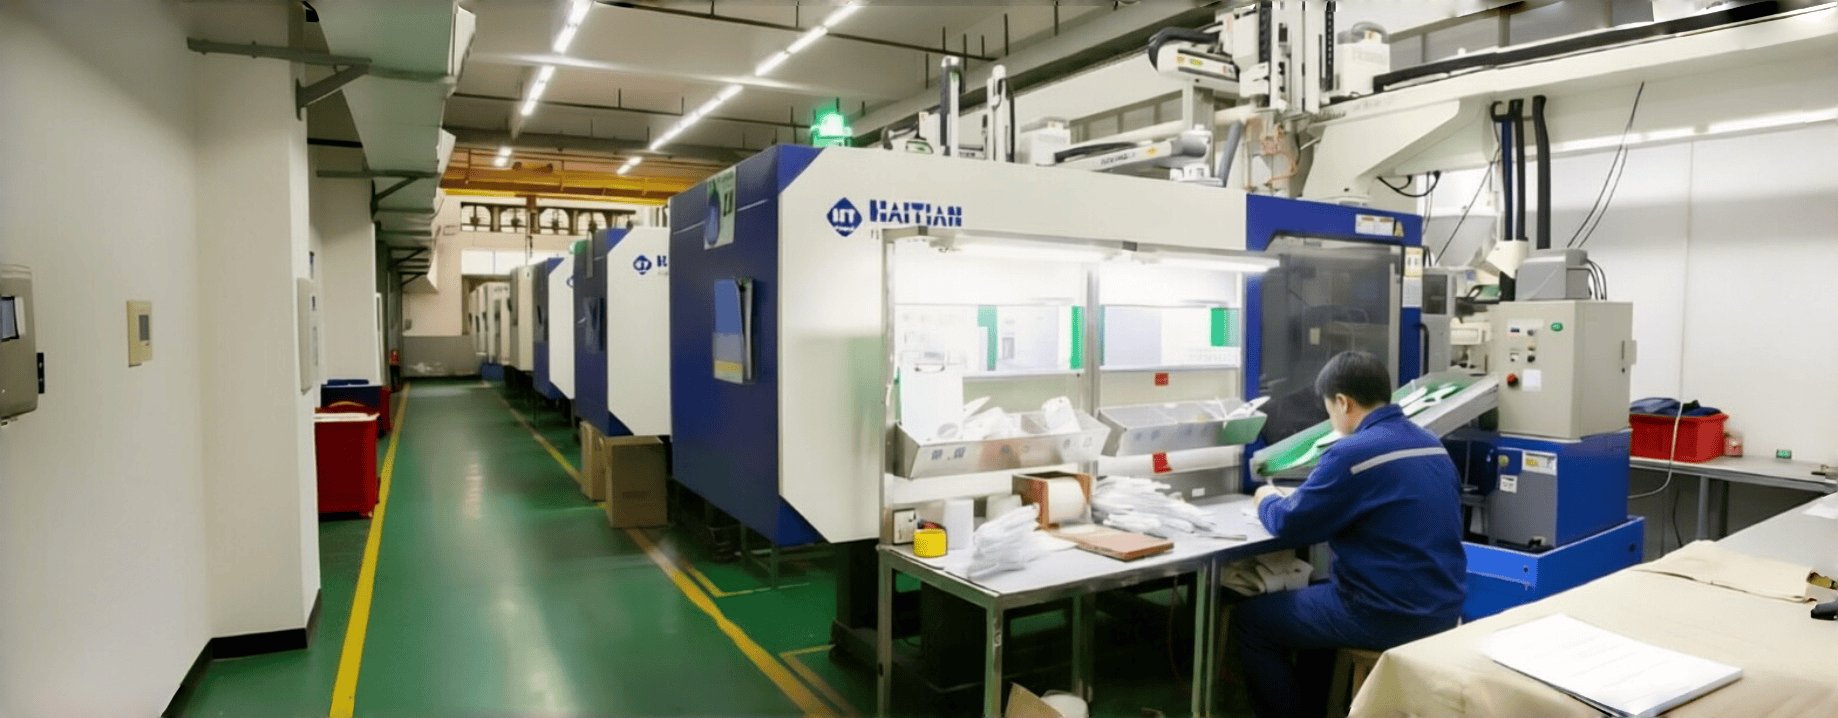
The plastic threaded cap is produced through precision injection molding using a 1x16 multi-cavity mold. This configuration uses a balanced runner system to ensure uniform filling of all 16 hexagonal heads, threaded cavities, and sealing rims simultaneously. Process parameters (melt temperature, injection pressure, cooling time) are strictly controlled to achieve dimensional accuracy, thread quality, and structural integrity across all cavities.
3. Thread Forming
The female threaded ends are formed directly in the mold using precision-machined thread inserts (cores). The thread profile (BSP, NPT, or Metric) is replicated with high accuracy to ensure proper fit and sealing with mating components. For a 1x16 mold, automatic unscrewing mechanisms or collapsible cores are essential to streamline the simultaneous removal of all 16 threaded cores.
4. Cooling & Ejection
The molded parts are cooled uniformly using an optimized cooling system to prevent warpage and shrinkage, particularly around the threaded areas. Ejection uses a stripper sleeve or ejector pins with proper draft angles to prevent drag marks or stress whitening, especially on the threads and sealing surfaces.
5. Post-Processing & Inspection
The parts are deflashed, inspected for dimensional accuracy (thread pitch, diameter, length), and tested for pressure resistance and sealing performance. Markings (size, material, pressure rating) are applied as required.
6. Packaging & Delivery
Finished caps are usually bulk packed or individually packed to prevent damage during transport. Packaging options include poly bags, blister packs, or custom cartons. We ship products by sea or air, depending on customer requirements.
Cost Advantage: 1x16 Multi-Cavity vs. 1x1 Single-Cavity
Choosing a 1x16 multi-cavity mold over a 1x1 single-cavity mold dramatically reduces per-unit manufacturing costs, which is critical for high-volume production of items like threaded caps.
| Cost Factor | 1x1 Single-Cavity Mold | 1x16 Multi-Cavity Mold | Cost Advantage |
|---|---|---|---|
| Labor Cost | Operator tends to one part per cycle | Operator tends to 16 parts per cycle | Labor cost per part drops by ~94% |
| Energy Consumption | Same power draw for 1 part | Same power draw for 16 parts | Energy cost per part drops by ~94% |
| Mold Cost Amortization | Low initial tooling cost | Higher initial tooling cost | Tooling cost per part becomes negligible at high volumes |
| Production Speed | Low output (e.g., 100 pcs/hr) | High output (e.g., 1,600 pcs/hr) | Faster order fulfillment and lower inventory costs |
While the initial investment for a 1x16 mold is higher, the cost per part drops sharply because you share machine time, labor, and energy. For mass production of threaded caps, the 1x16 configuration delivers the lowest total cost of ownership.
Manufacturing Difficulties & Countermeasures
1. Thread Quality & Dimensional Accuracy
| Item | Description |
|---|---|
| Challenge | Internal threads may have incomplete threads, flash, or dimensional deviation, causing leakage or difficulty in installation. |
| Root Cause | Mold wear; insufficient injection pressure; improper mold temperature; poor venting at thread areas; unscrewing speed out of sync. |
| Countermeasure | Use hardened steel inserts for thread molds; optimize venting; maintain consistent mold temperature; implement in-process thread gauging (GO/NO-GO gauges); sync unscrewing speed with mold opening. |
2. Hexagonal Body Warpage & Sink Marks
| Item | Description |
|---|---|
| Challenge | The hexagonal head or thick sections tend to warp or develop sink marks during cooling due to uneven wall thickness between the head and the threaded body. |
| Root Cause | Uneven cooling rates; inconsistent wall thickness; insufficient packing pressure; high injection speed. |
| Countermeasure | Optimize mold design with balanced cooling channels; use CAE simulation to predict shrinkage; increase packing pressure and time; adjust gate location for uniform flow; design generous fillets at corners. |
3. Weld Lines & Flow Marks
| Item | Description |
|---|---|
| Challenge | Weld lines and flow marks may appear on the surface, reducing appearance quality and potentially causing structural weakness. |
| Root Cause | Flow fronts meeting at low temperature; insufficient mold temperature; low injection speed; poor gate location. |
| Countermeasure | Increase mold temperature; optimize injection speed profile; adjust gate location to avoid weld lines in critical areas; use sequential valve gating if multi-cavity. |
4. Ejection Marks & Stress Whitening
| Item | Description |
|---|---|
| Challenge | Drag marks, ejection marks, or stress whitening may appear on the surface during ejection, especially on the smooth sealing surfaces and threads. |
| Root Cause | Insufficient draft angle; rough mold surface; excessive ejection force; insufficient cooling before ejection. |
| Countermeasure | Maintain draft angles of 1.5–3°; polish cavity surfaces to SPI A1–A2; use stripper sleeves or air-assisted ejection; optimize ejection speed and force; ensure adequate cooling time. |
5. Material Degradation (PVC/CPVC)
| Item | Description |
|---|---|
| Challenge | PVC and CPVC are temperature-sensitive and prone to degradation, causing discoloration and reduced mechanical properties. |
| Root Cause | Excessive melt temperature; long residence time in barrel; insufficient purging. |
| Countermeasure | Maintain melt temperature within recommended range (PVC: 170–190°C; CPVC: 190–210°C); use zone-by-zone barrel temperature control; purge regularly; avoid excessive residence time. |
6. Internal Thread Core Pulling & Deformation (Critical for 1x16)
| Item | Description |
|---|---|
| Challenge | The female threaded section may deform or become out-of-round during core pulling (unscrewing), affecting thread fit and sealing. In a 1x16 mold, any misalignment in one cavity affects the entire batch. |
| Root Cause | Insufficient cooling; excessive ejection force; mold wear; unscrewing speed too fast; uneven torque distribution across 16 cores. |
| Countermeasure | Optimize cooling around female thread; use roundness gauges for in-process inspection; maintain consistent packing pressure; use a synchronized rack-and-pinion or gear-driven unscrewing system to ensure all 16 cores rotate uniformly; replace worn mold inserts. |
7. Mold Balance & Short Shots (Specific to 1x16)
| Item | Description |
|---|---|
| Challenge | With 16 cavities, some parts may be short-shot or have inconsistent density due to unbalanced filling. |
| Root Cause | Uneven runner system; temperature differences across the mold; improper gate sizing. |
| Countermeasure | Use Mold Flow Analysis (CAE) to design a balanced runner system; implement hot runner systems with valve gates for precise control; maintain uniform mold temperature across all 16 cavities. |
Our Workflow
A transparent, step-by-step process from design to delivery — tailored for 1x16 multi-cavity plastic threaded caps & plugs.
Stage 1 — Inquiry & Drawing Review
Send us your drawing or a sample of the threaded plug/cap. We review dimensions, material requirements, thread specifications (BSP, NPT, Metric), pressure ratings, and connection type (female threaded cap, male threaded plug, or smooth masking cap) within 24 hours. We also evaluate the target annual volume to confirm whether a 1x16 multi-cavity mold is the most cost-effective solution for your project.
Stage 2 — DFM Report
Our engineers provide a Design-for-Manufacturability report, highlighting potential issues such as thread quality, hexagonal head warpage and sink marks at the thick head-to-body transition, ejection marks on sealing surfaces, and internal thread deformation during core pulling. For a 1x16 mold, we specifically analyze runner balance across all 16 cavities, synchronized unscrewing torque distribution, and cooling uniformity to prevent short shots and dimensional inconsistency. We suggest optimizations to improve moldability and reduce per-part cost.
Stage 3 — Mold Design & Fabrication
We design the 1x16 multi-cavity mold in SolidWorks, simulate filling, packing, and cooling with Moldflow to ensure balanced flow to all 16 cavities, and machine the mold in-house with precision thread inserts, synchronized automatic unscrewing mechanisms (rack-and-pinion or gear-driven), and optimized cooling channels for the hexagonal heads and threaded bodies (lead time: 30–40 days for a 1x16 mold).
Stage 4 — Sampling & Approval
We produce T1 samples from all 16 cavities, send them with inspection reports (dimensional, thread gauge GO/NO-GO, pressure test, leak test, roundness inspection, cavity-to-cavity consistency report), and iterate until you approve. We verify that every cavity produces parts within the same tolerance band before mass production.
Stage 5 — Mass Production & Shipping
Once approved, we begin mass production with full SPC monitoring and 100% pressure testing. With 16 parts per cycle, our output is up to 16 times higher than a single-cavity mold, dramatically shortening lead time and lowering unit cost — typical lead time: 15–20 days after approval.
Why Choose Yixing Technology?
Partner with a trusted leader in high-volume 1x16 multi-cavity plastic threaded cap & plug manufacturing.
20+ Years of Experience
Specialized in injection molding and precision thread forming since 2003. We have completed 5,000+ custom fitting, adapter, and threaded cap/plug projects.
Extensive experience in molding PVC, CPVC, PP, Nylon, and PVDF threaded caps and plugs with hexagonal heads, knurled bodies, and BSP, NPT, and Metric threads. Proven expertise in 1x16 multi-cavity molds with synchronized unscrewing systems for high-volume production.
ISO 9001:2015 Certified
Full quality management system with traceable production records for every batch.
We inspect each plastic threaded cap/plug batch for dimensional accuracy, thread quality, pressure resistance, sealing performance, and internal-thread roundness — including cavity-to-cavity consistency across all 16 cavities.
One-Stop Service
From material sourcing → mold design → injection molding → thread forming → inspection → packaging, all under one roof in our Shanghai factory.
Cost Advantage of 1x16 Multi-Cavity Production
By running 16 parts per cycle instead of 1, we reduce machine time, labor, and energy costs per part by up to 94%.
While the initial tooling investment is higher than a 1x1 mold, the cost per plug/cap drops exponentially at high volumes, giving you the lowest total cost of ownership for mass production.
Start Your Quote Here
CATEGORIES
LATEST NEWS
CONTACT US
- Mobile: +8615000908770
- Tel: +86-21-51662821
- WhatsApp: 8615000908770
- Email: contact@yx-molding.com
- Address: Room 323, Building B, Hongchun Business Park, No. 980 Qinghewan Road, Qingpu District, Shanghai