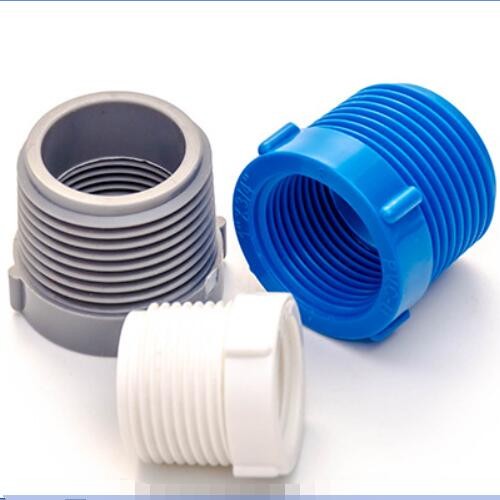
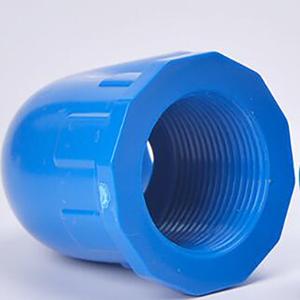
Female Pressure Pipes PVC Pipe Fittings / PVC Thread Pipe Fitting
Processing Capabilities for Plastic Threaded Adapters
| Item | Detailed Capabilities |
|---|---|
| Material (Housing) | PVC, CPVC, PP, Nylon (PA6/PA66), PVDF, ABS, PE, or custom engineering plastics |
| UV Stability | UV-stabilized options available for outdoor applications (PVC, CPVC, PP) |
| Shape / Style | Hexagonal body, round body with hand-tightening tabs/ribs, reducing adapter, straight adapter, male-female, male-male, female-female |
| Connection Type (End 1) | Male Threaded (BSP, NPT, Metric), Female Threaded, Socket (solvent weld), Flange, Hose Barb |
| Connection Type (End 2) | Female Threaded, Male Threaded, Socket (solvent weld), Flange, Hose Barb |
| Port Size | 1/4" to 4" (DN8–DN100), custom sizes available |
| Thread Standard | BSP (G), NPT, Metric (M), or custom thread profiles |
| Pressure Rating | 0.6–1.6 MPa (6–16 bar), depending on material and design |
| Operating Temperature | -20°C to 95°C (depending on material: PVC 0–60°C, CPVC 0–95°C, PP 0–90°C, Nylon -40–120°C) |
| Sealing Method | Thread sealant (PTFE tape), O-ring, gasket, or solvent welding |
| Surface Finish | Smooth, textured, or custom finishes available |
| Color | Grey, white, blue, black, or custom colors matched to customer requirements |
| Marking | Size, material, pressure rating, or custom markings molded or printed on body |
| Processing Tolerance | Thread tolerance ±0.1mm, Diameter tolerance ±0.1mm, Length tolerance ±0.5mm |
| Certifications | ISO9001, ROHS, CE, NSF, food-grade options available |
| Applications | Water treatment, irrigation, plumbing, chemical processing, HVAC, marine, aquarium, and industrial fluid handling |
Injection Molding Process for Plastic Threaded Adapters
1. Raw Material Preparation
High-quality PVC, CPVC, PP, Nylon (PA6/PA66), or PVDF pellets are selected based on the application requirements (pressure, temperature, chemical compatibility). The raw material is dried (for Nylon and PP) and pre-conditioned to remove moisture, ensuring optimal molding performance and preventing surface defects like silver streaks or bubbles.
2. Injection Molding
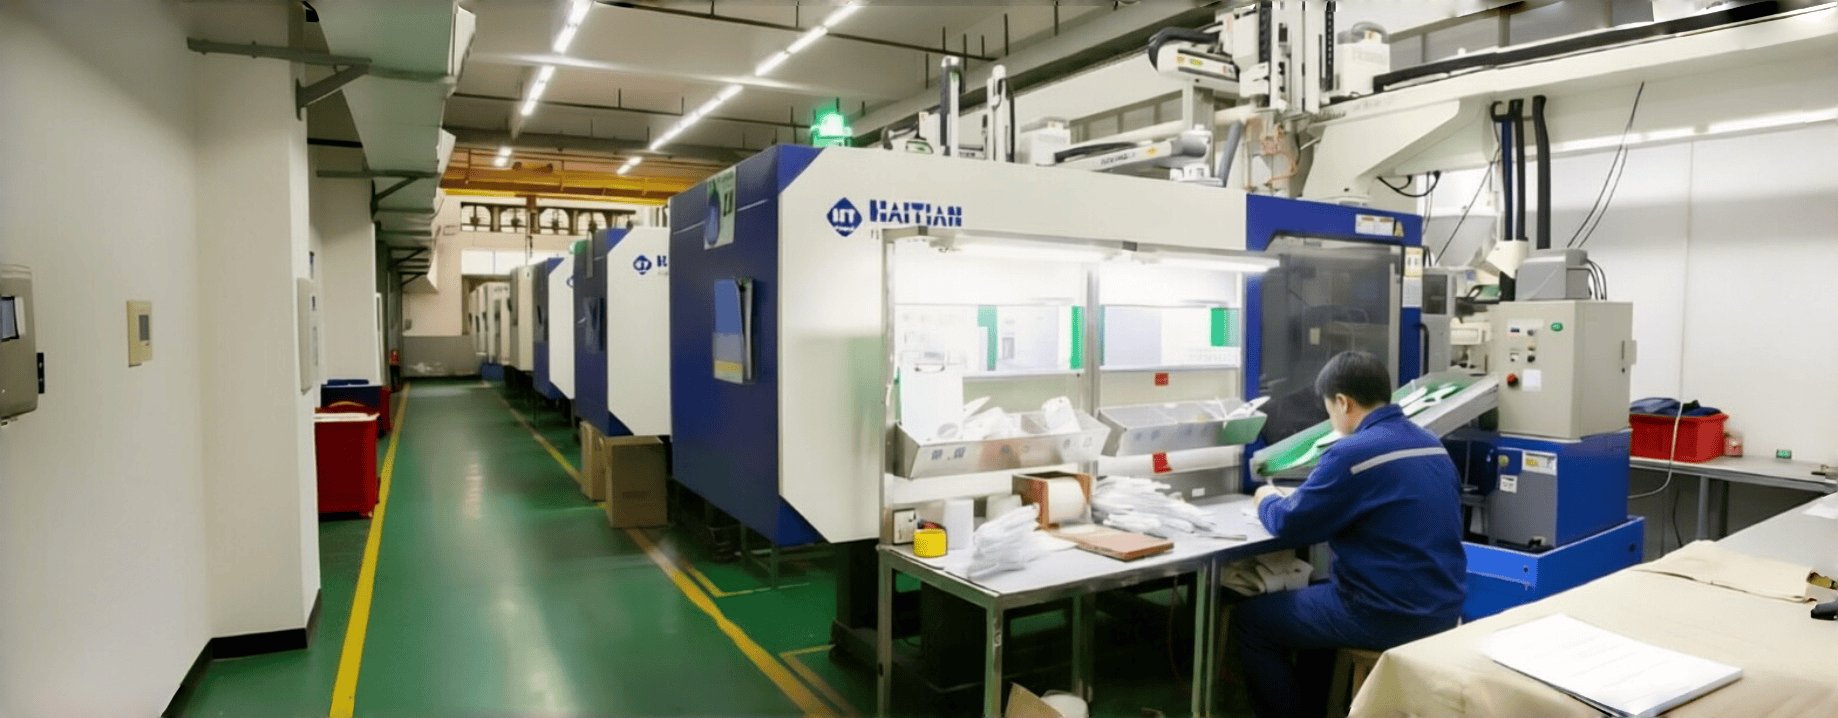
The plastic threaded adapter is produced through precision injection molding. The mold is designed with a balanced runner system to ensure uniform filling of the hexagonal body, male threaded end, female threaded end, and hand-tightening tabs. Process parameters (melt temperature, injection pressure, cooling time) are strictly controlled to achieve dimensional accuracy, thread quality, and structural integrity.
3. Thread Forming
Both male and female threaded ends are formed directly in the mold using precision-machined thread inserts. The thread profile (BSP, NPT, or Metric) is replicated with high accuracy to ensure proper fit and sealing with mating components. Automatic unscrewing mechanisms are used for high-volume production.
4. Cooling & Ejection
The molded part is cooled uniformly using an optimized cooling system to prevent warpage and shrinkage. Ejection is performed using a stripper sleeve or ejector pins with proper draft angles to prevent drag marks or stress whitening on the surface, especially on the threads and sealing surfaces.
5. Post-Processing & Inspection
The part is deflashed, inspected for dimensional accuracy (thread pitch, diameter, length), and tested for pressure resistance and sealing performance. Markings (size, material, pressure rating) are applied as required.
6. Packaging & Delivery
Finished adapters are individually packed to prevent damage during transport. Packaging options include poly bags, blister packs, or custom cartons. Products are shipped by sea or air according to customer requirements.
Manufacturing Difficulties & Countermeasures
1. Thread Quality & Dimensional Accuracy
| Item | Description |
|---|---|
| Challenge | Male and female threads may have incomplete threads, flash, or dimensional deviation, causing leakage or difficulty in installation. |
| Root Cause | Mold wear; insufficient injection pressure; improper mold temperature; poor venting at thread areas; unscrewing speed out of sync. |
| Countermeasure | Use hardened steel inserts for thread molds; optimize venting; maintain consistent mold temperature; implement in-process thread gauging (GO/NO-GO gauges); sync unscrewing speed with mold opening. |
2. Hexagonal Body & Tab Warpage
| Item | Description |
|---|---|
| Challenge | The hexagonal body or hand-tightening tabs tend to warp or deform during cooling due to uneven wall thickness and sharp corners. |
| Root Cause | Uneven cooling rates; inconsistent wall thickness; insufficient packing pressure; high injection speed. |
| Countermeasure | Optimize mold design with balanced cooling channels; use CAE simulation to predict shrinkage; increase packing pressure and time; adjust gate location for uniform flow; design generous fillets at corners. |
3. Weld Lines & Flow Marks
| Item | Description |
|---|---|
| Challenge | Weld lines and flow marks may appear on the surface, reducing appearance quality and potentially causing structural weakness. |
| Root Cause | Flow fronts meeting at low temperature; insufficient mold temperature; low injection speed; poor gate location. |
| Countermeasure | Increase mold temperature; optimize injection speed profile; adjust gate location to avoid weld lines in critical areas; use sequential valve gating if multi-cavity. |
4. Ejection Marks & Stress Whitening
| Item | Description |
|---|---|
| Challenge | Drag marks, ejection marks, or stress whitening may appear on the surface during ejection, especially on the smooth sealing surfaces and threads. |
| Root Cause | Insufficient draft angle; rough mold surface; excessive ejection force; insufficient cooling before ejection. |
| Countermeasure | Maintain draft angles of 1.5–3°; polish cavity surfaces to SPI A1–A2; use stripper sleeves or air-assisted ejection; optimize ejection speed and force; ensure adequate cooling time. |
5. Material Degradation (PVC/CPVC)
| Item | Description |
|---|---|
| Challenge | PVC and CPVC are temperature-sensitive and prone to degradation, causing discoloration and reduced mechanical properties. |
| Root Cause | Excessive melt temperature; long residence time in barrel; insufficient purging. |
| Countermeasure | Maintain melt temperature within recommended range (PVC: 170–190°C; CPVC: 190–210°C); use zone-by-zone barrel temperature control; purge regularly; avoid excessive residence time. |
6. Female Thread Core Pulling & Deformation
| Item | Description |
|---|---|
| Challenge | The female threaded end may deform or become out-of-round during core pulling, affecting thread fit and sealing. |
| Root Cause | Insufficient cooling; excessive ejection force; mold wear; unscrewing speed too fast. |
| Countermeasure | Optimize cooling around female thread; use roundness gauges for in-process inspection; maintain consistent packing pressure; sync unscrewing speed with mold opening; replace worn mold inserts. |
Our Workflow
Stage 1 — Inquiry & Drawing Review
You send us your drawing or sample. We review dimensions, material requirements, thread specifications (BSP, NPT, Metric), pressure ratings, and connection type (male/female/socket) within 24 hours.
Stage 2 — DFM Report
Our engineers provide a Design-for-Manufacturability report, highlighting potential issues such as thread quality, hexagonal body warpage, sink marks on thick sections, ejection marks on sealing surfaces, and female thread deformation, and suggesting optimizations for moldability and cost.
Stage 3 — Mold Design & Fabrication
We design the mold in SolidWorks, simulate filling and cooling with Moldflow, and machine the mold in-house with precision thread inserts, automatic unscrewing mechanisms, and optimized cooling channels for hexagonal bodies and hand-tightening tabs (lead time: 25–35 days).
Stage 4 — Sampling & Approval
We produce T1 samples, send them with inspection reports (dimensional, thread gauge GO/NO-GO, pressure test, leak test, roundness inspection), and iterate until you approve.
Stage 5 — Mass Production & Shipping
Once approved, we begin mass production with full SPC monitoring and 100% pressure testing. Typical lead time: 15–20 days after approval.
Why Choose Yixing Technology?
20+ Years Experience
Specialized in injection molding and precision thread forming since 2003. We have completed 5,000+ custom fitting and adapter projects.
Extensive experience in molding PVC, CPVC, PP, Nylon, and PVDF threaded adapters with hexagonal bodies, hand-tightening tabs, and BSP, NPT, and Metric threads.
ISO 9001:2015 Certified
Full quality management system with traceable production records for every batch.
We inspect each plastic threaded adapter batch for dimensional accuracy, thread quality, pressure resistance, sealing performance, and roundness of female threads.
One-Stop Service
From material sourcing → mold design → injection molding → thread forming → inspection → packaging, all under one roof in our Shanghai factory.
From precision thread inserts and hexagonal body molding to pressure testing and global shipping — all under one roof.
Start Your Quote Here
CATEGORIES
LATEST NEWS
CONTACT US
- Mobile: +8615000908770
- Tel: +86-21-51662821
- WhatsApp: 8615000908770
- Email: contact@yx-molding.com
- Address: Room 323, Building B, Hongchun Business Park, No. 980 Qinghewan Road, Qingpu District, Shanghai