One-Stop Solutions for Complex Lamp Covers
Lamp covers typically feature complex geometries, including deep cavities, multi-step rotational bodies, and sharp corners, which demand multi-stage precision deep-drawing dies. Yixing Technology brings over 20 years of expertise to these challenges. We don't just manufacture molds—we provide comprehensive manufacturing solutions to accelerate your prototyping and reduce overall costs.
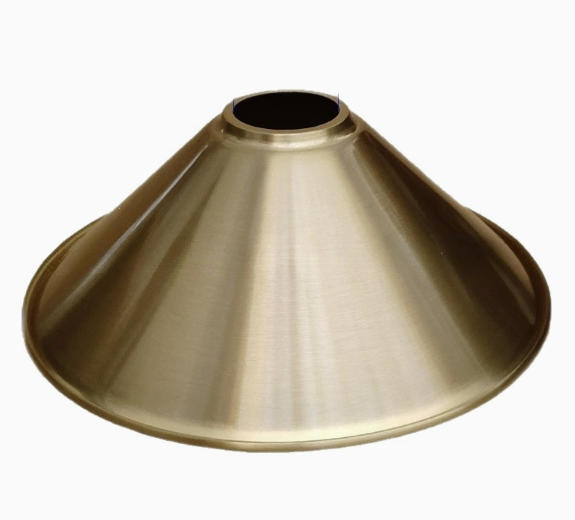
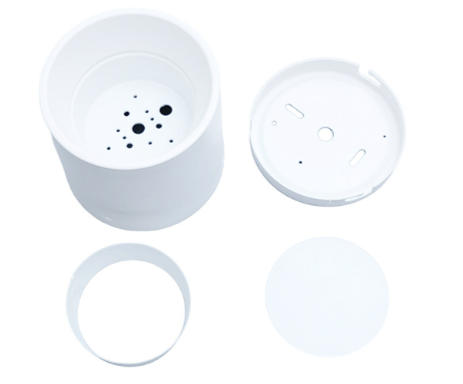
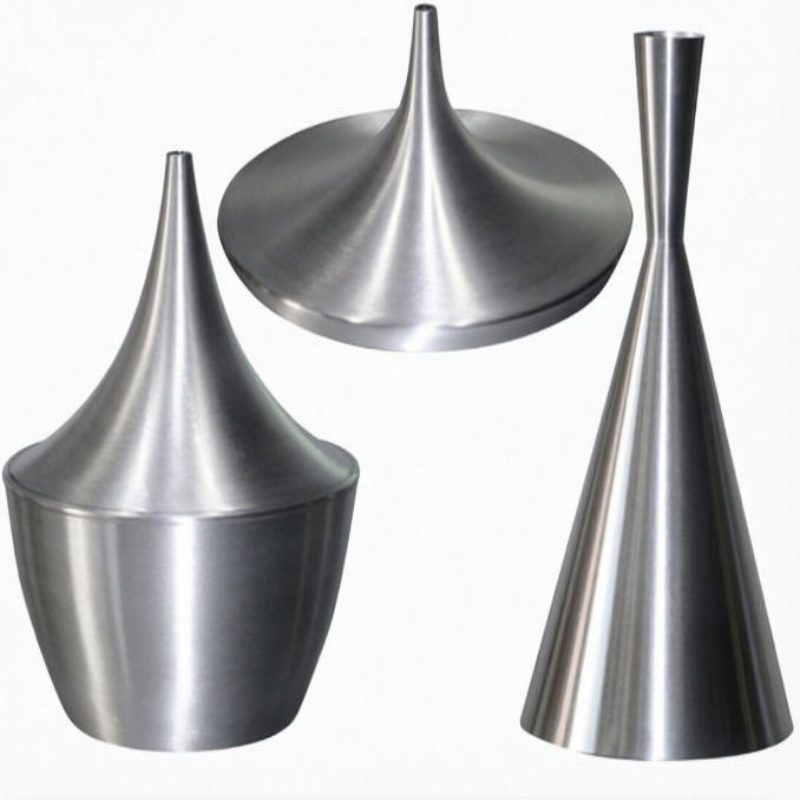
Metal Lamp Shade Shell Capably
| Parameter | Specification |
|---|---|
| Applicable Materials | Aluminum alloy (5052 / 6061), Low-carbon steel (SPCC / SECC), Stainless steel (SUS304), Copper alloy (Brass / Phosphor bronze) |
| Sheet Thickness Range | 0.3–10.0 mm |
| Drawing Ratio (D/d) | 1.5–2.2 (first draw); 1.2–1.5 (subsequent draws) |
| Dimensional Tolerance | ±0.05 mm (typical); ±0.02 mm (precision) |
| Roundness | ≤ 0.05 mm |
| Flatness | ≤ 0.05 mm / 100 mm |
| Process Types | Multi-station deep drawing (4–8 stations) / Metal spinning |
| Die Steel | SKD11, DC53, Tungsten carbide (YG20 / YC20C) |
| Die Life | ≥1,000,000 strokes (deep drawing); ≥500,000 pcs (spinning mandrel) |
| Stamping Speed | 30–120 SPM (deep drawing); 200–800 RPM (spinning) |
| Press Tonnage Range | 50T–400T |
| Surface Roughness (Lighting Parts) | Ra ≤ 0.4 µm (mirror finish); Ra ≤ 0.8 µm (satin) |
Material We support
| Material | Typical Grade | Thickness Range | Characteristics |
| Aluminum Alloy | 5052 / 6061 | 0.5–10.0 mm | Lightweight, corrosion-resistant, good formability |
| Low-Carbon Steel | SPCC / SECC | 0.3–6 mm | Good formability, low cost, weldable |
| Stainless Steel | SUS304/SUS 316 | 0.3–6mm | Corrosion resistance, high strength, work-hardening |
| Copper Alloy | Brass / Phosphor bronze | 0.3–10.0 mm | Good conductivity, excellent formability, premium look |
Process Comparison
1. Deep Drawing Mold (High Volume)
Lamp covers require continuous deep drawing through multiple die sets (typically 4–8 stations) to form flat sheets into complex deep-cavity shapes. How we can get the top quality parts?
1) Reasonable Process Design
The deformation amount for each stage is precisely calculated to balance material flow, preventing wrinkling and cracking from the very beginning of the design phase.
2) High-Rigidity Mold Steel
Dies are manufactured from extremely high structural rigidity steel to prevent elastic deformation during stamping, ensuring superior surface precision.
3) Optimized Mold Clearance
The gap between punch and die is uniformly controlled—slightly larger than material thickness—to ensure smooth material flow without excessive thinning.
4) Wrinkle & Crack Prevention
We utilize advanced deep-drawing processes, high-performance oils, process supplements, and drawing ribs to balance flat-area wrinkling and corner cracking.
5) Flawless Surface Finish on Formed Lamp Cover
Defect-Free Surface Quality – Free from Scoring or Die Marks
2. Metal Spinning (Small Quantities)
Understanding that tooling costs and lead times are critical, we offer metal spinning services for lamp covers. This allows us to produce complex parts without heavy investment in tooling.
1) Cost-Effective and more Flexibility
Metal spinning achieves deep-cavity shapes similar to deep drawing but eliminates expensive die costs entirely.
2) Fast Test
Go from CAD model to physical part in days, not weeks—perfect for prototyping and low-volume production.
| Comparison Item | Deep Drawing | Metal Spinning |
| Tooling Cost | High | Very low |
| Unit Cost | Very low (high-speed stamping) | Relatively high |
| Best For | High volume (100K+) | Low volume /(100-10k) |
| Lead Time | 6–10 weeks | A few days |
| Precision | ±0.05 mm | ±0.1–0.3 mm |
Our Process Flow
1. Deep drawing die For high quantity :
DFM Design → Die Manufacturing (CNC / Wire EDM / EDM) → Die Assembly → Trial Run (T1) → Small-Batch Validation → Mass Production
1) DFM – Review drawings, shell geometry, draw ratio, stations, clearance, springback.
2) Die Manufacturing – CNC, wire EDM, sinker EDM, grinding, heat treatment, coating, inspection.
3) Die Assembly – Assemble plates, punches, dies, pilots, springs; set clearance and feed.
4) Trial Run (T1) – Mount die, run samples, check dimensions, roundness, flatness, surface; adjust.
5) Small Batch – 500–5,000 pcs; CPK/PPK, tool wear, polishing, PPAP approval.
6) Mass Production – High-speed deep drawing, SPC, maintenance, polishing, packaging.
2. Metal Spinning (Low Volume / Prototype):
DFM Design → Mandrel Manufacturing → Spinning → Trimming → Surface Finishing → Inspection → Shipment
1) DFM – Review drawings, shell geometry, spinning feasibility, material.
2) Mandrel Manufacturing – CNC turning, polishing, heat treatment.
3) Spinning – Mount blank, spin at 200–800 RPM, form against mandrel.
4) Trimming – Cut to final height, edge deburring.
5) Surface Finishing – Polishing, anodizing, painting, brushing.
6) Inspection – Dimensions, roundness, surface roughness.
7) Shipment – Packing and delivery.
Why Choose Us?
Our molds are engineered using premium materials such as SKD11, DC53, and tungsten carbide, ensuring stable performance and long service life—even under high-volume deep drawing and spinning production.
- Forming Components (punches & dies) – Precision-ground to maintain exact shell geometry and minimal die clearance.
- Positioning Systems (pilot pins, stop pins) – Ensure consistent material alignment stroke after stroke.
- Guiding Systems (guide posts, bushings) – Maintain alignment and reduce wear during high-speed operation.
- Support Structures – Provide the rigid framework essential for precision forming.
ISO/TC 29/SC 8, DIN ISO 18084, VDI 3357, VDI 3386, VDI 3349, and ANSI B5.25 can be used in mold design, making repair and maintenance easier.
We offer both multi-station deep drawing for high-volume production and metal spinning for low-volume or prototype runs—giving you the right process for every project.
For lamp shades, we achieve mirror-polished surfaces (Ra ≤ 0.4 µm) with no orange peel, scratches, or tool marks—meeting the highest appearance standards.
We are an ISO-certified company with a strict quality control system, designing and manufacturing molds strictly according to customer requirements. We provide one-stop stamping solutions combining high stability, competitive pricing, and reliable performance. We look forward to putting our expertise to work for you.
FAQ
Send Your Message
Feel free to contact us. We are ready to assist you.
Start Your Quote Here
CATEGORIES
LATEST NEWS
CONTACT US
- Mobile: +8615000908770
- Tel: +86-21-51662821
- WhatsApp: 8615000908770
- Email: contact@yxplasticmolding.com
- Address: Room 323, Building B, Hongchun Business Park, No. 980 Qinghewan Road, Qingpu District, Shanghai