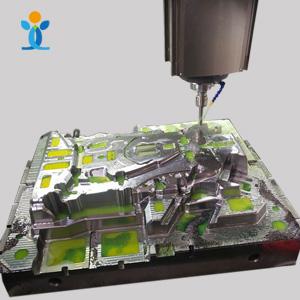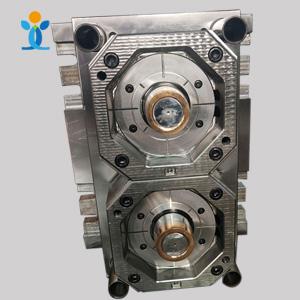
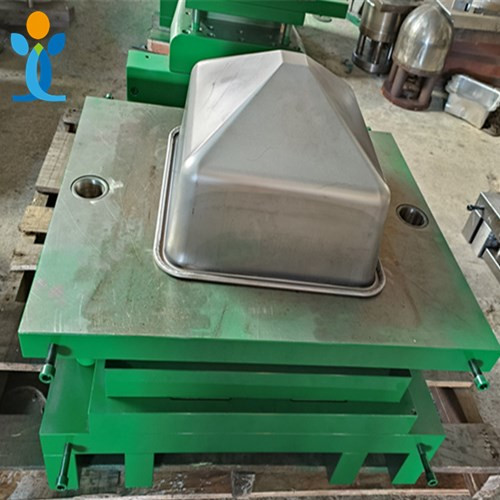
This single-station deep drawing die produces hopper-shaped components — tapered parts with a large, flat mounting flange (we also make similar parts such as funnels, feed hoppers, filter housings, containers, or industrial covers). Each die performs one specific drawing operation, requiring specialized techniques to control material flow into the tapered body.
Built with DC53 / SKD11 / Cr12MoV tool steel for high wear resistance and toughness, the die is rated for approximately 300,000 – 800,000 strokes. It runs on a 1500 kN press with manual transfer between dies, deep drawing DC04, SPCC, SPHC, SUS304, aluminum, copper or brass at 1.2 mm thickness (0.6–5.0 mm acceptable) and tolerances down to ±0.20 mm for flange flatness and body taper.
Technical Specifications
Key Features of This Mold (Hopper-Shaped Deep Drawing)
1. Single-Station Design with Tapered Punch
Each die performs one specific drawing operation (first draw, second draw, reshaping). The tapered punch creates the hopper’s sloped walls, and the part is transferred manually to the next die for successive drawing stages.
2. Heavy-Duty Guide System
Four large guide pillars with helical springs maintain perfect alignment between the upper and lower die halves — essential for hopper-shaped parts with large flanges to ensure uniform wall thickness and prevent flange wrinkling.
3. Complex Inserts & Drawing Punches
The die contains tapered drawing punches, dies, and blank holders. The modular design makes maintenance easier — if one drawing section wears out, you replace only that insert, not the entire die block.
4. High-Quality Base and Structure
The high-quality steel base plate with lifting rings can resist vibration from a mechanical press to ensure long-term stability, even when deep drawing thicker materials.
5. Profiled Blank Holder Design
Blank holders control material flow and prevent wrinkling. In this hopper-shaped mold, the blank holder must match the tapered punch profile to ensure even pressure distribution across the part.
6. Large Flange Forming Area
The die features a wide, flat flange area requiring precise control of blank holder force — preventing flange wrinkling while allowing material to flow smoothly into the tapered body.
Manufacturing Process (Hopper-Shaped Deep Drawing)
Single-station deep drawing integrates one operation per die. The process flow for a hopper-shaped part usually follows this sequence.
1. Blanking
A circular or shaped blank is cut from the metal strip or sheet.
2. First Draw
The blank is drawn into a shallow hopper shape using a tapered drawing punch and die.
3. Second Draw
The hopper is drawn deeper — the tapered walls form and the flange develops.
4. Third Draw
Further drawing to achieve the final depth and taper angle.
5. Reshaping / Coining
A reshaping die corrects the shape, ensures dimensional accuracy and reduces springback.
6. Trimming
Any excess material or uneven edges (earing) are trimmed off to define the final flange outline.
7. Flanging / Piercing
Additional operations to create mounting holes or strengthen the flange if required.
Challenges & Solutions (Hopper-Shaped Deep Drawing)
1. Flange Wrinkling and Body Tearing
ChallengeThe large, flat flange is prone to wrinkling (compressive stress), while the tapered body walls are prone to tearing (excessive tensile stress).
SolutionUse a profiled blank holder with precise force control (springs or hydraulic cushions), optimize the drawing radius and clearance with AutoForm simulation, apply proper lubrication and consider drawing beads in the flange area.
2. Dimensional Accuracy and Taper Angle
ChallengeMaintaining the precise taper angle, flange flatness and height is difficult — parts often require ±0.20 mm tolerance and must be interchangeable.
SolutionUse high-precision guide pillars and bushings to keep the dies perfectly aligned, inspect drawing clearances regularly, and use CMM inspection for first-article and in-process verification.
3. Tool Wear and Life
ChallengeRepeated high-impact deep drawing wears the tapered drawing edges and forming surfaces, especially with thicker materials.
SolutionUse DC53 or SKD11 tool steel; proper deep-drawing lubrication extends die life by up to 30%. Apply TiCN / TiAlN coatings to punches and polish the drawing dies to a mirror finish.
4. Springback and Thickness Variance
ChallengeThe metal springs back after drawing, affecting the taper angle and flange flatness, and different material batches cause inconsistencies.
SolutionCompensate for springback at design phase using AutoForm simulation, add a sizing station to correct the shape after forming, and run regular incoming-material quality checks.
5. Surface Finish and Lubrication
ChallengeDeep drawing generates friction and heat, causing galling, scratching or seizure on the part surface, especially on the tapered walls.
SolutionUse high-viscosity deep drawing lubricants, polish die surfaces to a mirror finish and apply TiCN / TiAlN coatings to drawing punches and dies; regularly lubricate and clean the die.
6. Blank Holder Force Control
ChallengeThe large flange requires precise blank holder force — too much causes tearing, too little causes wrinkling.
SolutionUse hydraulic cushions or nitrogen springs for adjustable blank holder force, optimize with AutoForm simulation, fine-tune during tryout, and consider segmented blank holders for complex hopper shapes.
Single-Station Deep Drawing Dies Advantage
High Precision
Ideal for tight-tolerance industrial parts held within ±0.20 mm.
Cost-Effective for Low Volume
Lower tooling cost than progressive dies for complex deep-drawn parts.
Flexibility
Easy to adjust or modify individual drawing stations independently.
Automation
Can be equipped with robotic transfer for continuous production.
Our Process (Hopper-Shaped Deep Drawing Parts)
Inquiry → DFM Analysis → Die Design → Die Manufacturing → Sample Approval → Small Batch Order → Mass Production → Shipping.
1. Inquiry
Customer provides part drawings, material specs (e.g., SPCC, SPHC, SUS304, SUS316), tolerance requirements and annual volume for the hopper-shaped part.
2. DFM Analysis (Design for Manufacturing)
Engineers analyze blank size, material utilization, drawing sequence and potential forming defects before designing the mold, then send optimization feedback.
3. Die Design
3D CAD design of the deep drawing die: tapered drawing punch and die block, guide pillar and spring system, profiled blank holder and ejection mechanism, and AutoForm simulation to predict springback, thinning and wrinkling.
4. Die Manufacturing
Material procurement (DC53, SKD11, etc.), CNC machining, wire EDM and grinding, heat treatment for punches and inserts, polishing of drawing dies to mirror finish, assembly and fitting, and spotting and tryout to industrial tolerance standards.
5. Sample Approval
Trial run on the press. First articles are measured and inspected using a CMM (Coordinate Measuring Machine), and samples are sent for dimensional and functional approval.
6. Small Batch Order
After sample approval, a small production batch verifies die stability, consistency and production speed.
7. Mass Production
Full-scale production with manual or robotic transfer, producing thousands of parts per hour. In-process inspection and SPC (Statistical Process Control) maintain quality.
8. Shipping
We pack, label and ship finished parts on schedule, offering custom packaging and traceability labels.
Why Choose Us for Deep Drawing Die Solutions?
Partner with a trusted leader in precision deep drawing die manufacturing.
20+ Years of Experience
Since 2006 we have produced more than 1,500 dies and stamped parts, including hopper-shaped parts, funnels, filter housings and industrial containers.
ISO 9001 Certified
Strict quality control system, providing ROHS / CE certification for your peace of mind.
One-Stop Service
Value-added operations simplify your supply chain from design to delivery, including welding, tapping, plating and powder coating.
In-House Die Manufacturing
Complete capability from DFM analysis and die design to machining, assembly and trial runs — all under one roof. No outsourcing delays.
High-Speed Production
Deep drawing dies designed for manual or robotic transfer, producing thousands of precision parts per hour.
Deep Drawing Expertise
Experience with high-strength materials, thick material and tapered drawing, and the critical requirements for dimensional consistency, surface finish and structural integrity in hopper-shaped applications.