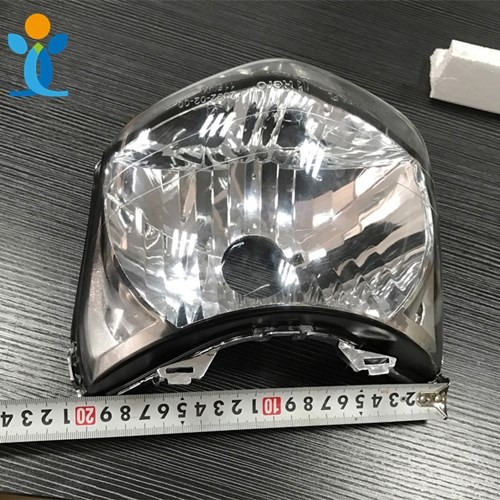
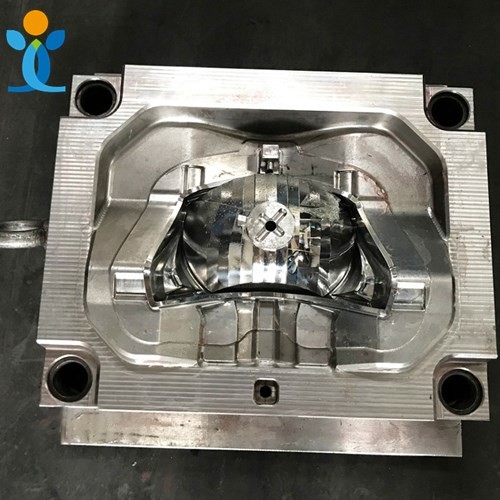
One large, high-value optical part per cycle — This 1x1 (single-cavity) injection mold is engineered to produce large automotive lighting components such as headlight outer lenses and complex inner light guides, with a deeply contoured, highly polished cavity for optical clarity and precise light diffusion.
Built on a custom heavy-duty steel base with S136 corrosion-resistant steel core and cavity, the mold is designed for PC and PMMA materials, delivering a mirror-grade optical surface, dimensional stability, and long mold life for demanding automotive applications.
A hot runner valve-gate system eliminates cold-runner waste and keeps a clean gate vestige, while Mold Flow Analysis (MFA) and an ISO 9001:2015 certified process guarantee balanced filling, controlled warpage and flawless optical finish.
Technical Specifications
Core Characteristics
Optical-Grade Surface Finish
The cavity is polished to a mirror-like finish (SPI A1-A2), critical for producing transparent PC or PMMA parts without distortion or light scattering.
Complex 3D Geometry
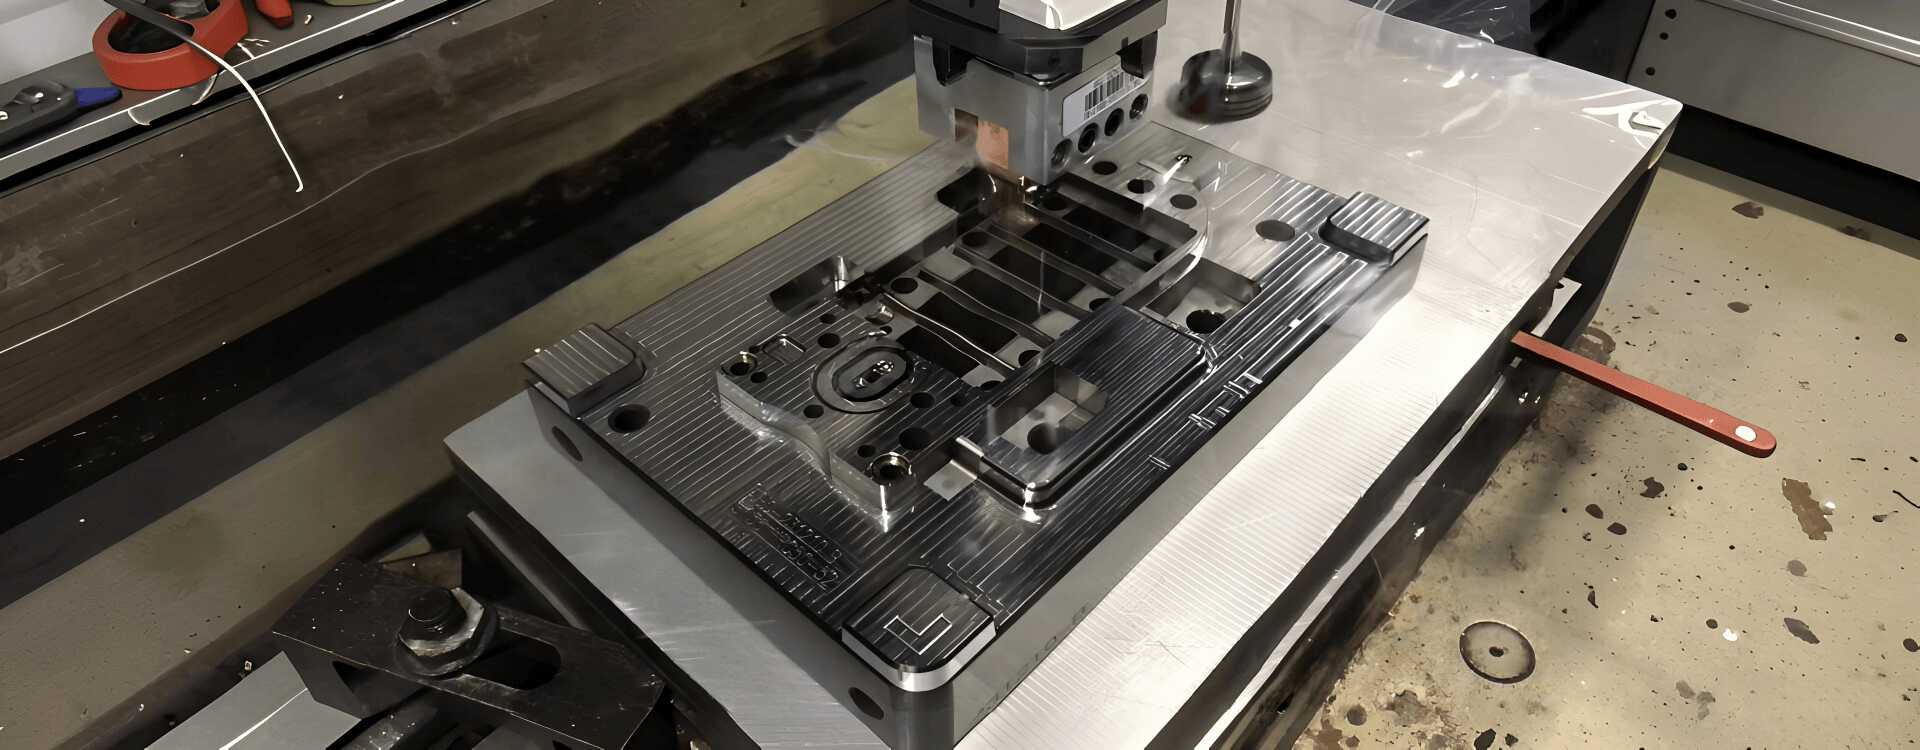
Deep, sweeping curves and an asymmetrical shape require advanced 3D machining and EDM processes to achieve perfect replication.
Single Large Cavity Efficiency
Designed for high-tonnage machines to produce one large, high-value part per cycle, minimizing assembly and secondary operations.
Robust Construction
Built to withstand the high injection pressures required to fill a large, thin-walled optical part without flashing.
Processing Difficulties & Countermeasures
1. Optical Surface Polishing (No Scratches or Flow Marks)
The deep, curved surfaces must be polished to a flawless mirror finish. Any micro-scratch, EDM recast layer, or flow mark causes light distortion or visible defects on the final car light.
High-speed CNC machining followed by precision EDM with fine electrode tolerances; hand-polishing with diamond paste and ultrasonic polishing to reach SPI A1-A2; optimized gate location and injection speed to eliminate weld lines.
2. Deep Cavity & Uniform Cooling
The deep, asymmetrical shape makes it hard to place cooling channels close to the part surface; uneven cooling leads to warpage, sink marks, and long cycle times.
Conformal or baffled cooling channels follow the part curvature; Mold Flow Analysis (MFA) simulates the cooling process to ensure uniform temperature across the entire lens.
3. High Injection Pressure & Clamping Force
Filling a large, thin-walled optical part requires extremely high injection pressure; any mold weakness can cause flashing, deformation, or damage to the polished surface.
High-strength S136 steel for core and cavity; mold base reinforced with thick support plates and heavy-duty guide pins; high-tonnage injection machine with precise pressure control recommended.
4. Warpage & Shrinkage Control (PC/PMMA)
PC and PMMA have different shrinkage rates, and the large, curved geometry is prone to warping, affecting lens fitment on the car body.
Holding pressure and cooling time optimized during sampling; adjustable cooling zones fine-tune temperature distribution; CMM dimensional inspection ensures tight tolerances.
5. Ejection of Fragile Optical Parts
The large, thin lens can be fragile and easily cracked or deformed during ejection; standard ejector pins can leave marks on the optical surface.
Large-diameter sleeve ejectors or air-assisted ejection distribute force evenly; the ejection stroke is calibrated to prevent deformation; ejector pins are positioned on non-optical surfaces.
6. Gate Vestige & Cosmetic Defects
The gate location must be carefully chosen to ensure balanced filling and avoid visible flow marks on the lens surface.
Mold Flow Analysis determines the optimal gate location; for large lenses a hot runner valve gate system is recommended to eliminate cold runner waste and ensure a clean gate vestige.
Applicable Industries
Our Workflow
A transparent, step-by-step process from design to delivery.
R&D Support & DFM Analysis
We support customer R&D for automotive lighting components, creating or improving 3D files (UG, SolidWorks, ProE, AutoCAD, etc.), and provide a Mold Flow Analysis (MFA) report to optimize the optical geometry, gate location, and cooling layout.
Mold Process & Optical Integration
Mold design (DFM report) → check/approve → approved → make mold → integrate hot runner system → produce sample → sample confirmed → check final mold quality, ready to export. The cavity's optical clarity and surface finish are validated during this stage.
Sample Modification & Optical Optimization
If the first sample does not meet requirements (e.g. flow marks, warpage, or optical distortion), we modify the mold — fine-tuning gate sizes, cooling circuits and injection parameters to meet your exact optical requirements.
Sample Delivery
We produce the customer's requested quantity (typically 200-500 shots for validation), with free shipping.
Final Delivery
We deliver goods by sea or air, and can accommodate special requirements (such as custom heavy-duty crating for the large mold) based on customer needs.
Why Choose Us?
Partner with a trusted leader in precision injection molding.
20+ Years of Experience
More than 1,500 new injection molds and parts produced since 2006, with deep expertise in large-scale molds and optical-grade molds for the automotive lighting industry.
ISO 9001 Certificated
A strict quality control system with ROHS/CE certification. Every mold base and steel insert meets rigorous dimensional and optical standards.
One-Stop Service
Value-added operations simplify your supply chain from design to delivery — from Mold Flow Analysis to optical polishing and texture etching, we handle the technical complexity so you don't have to.