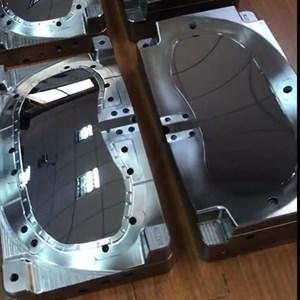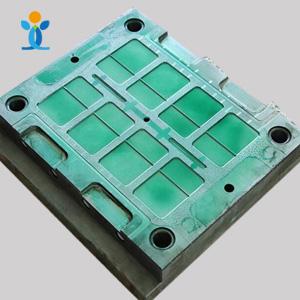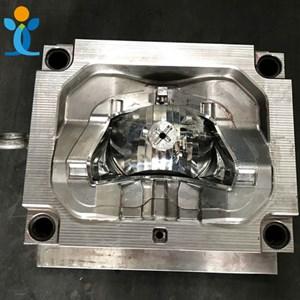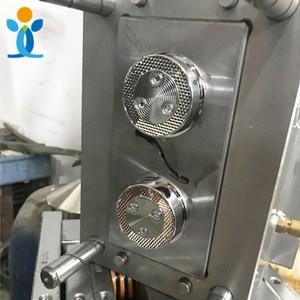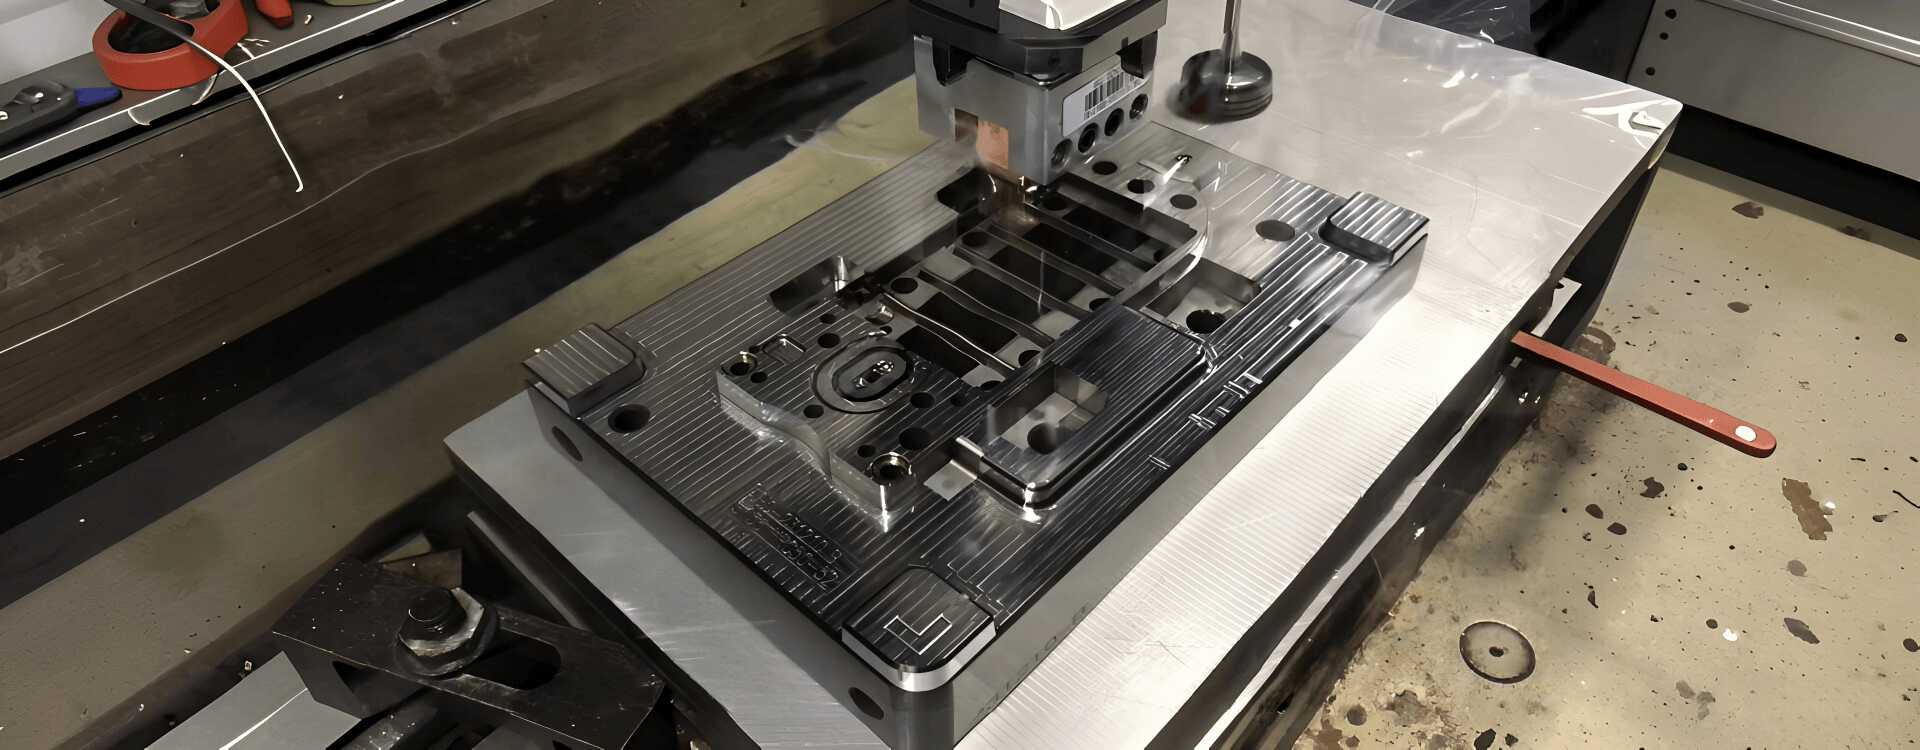
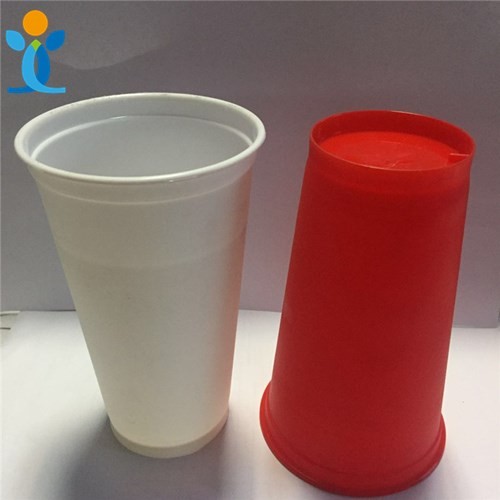
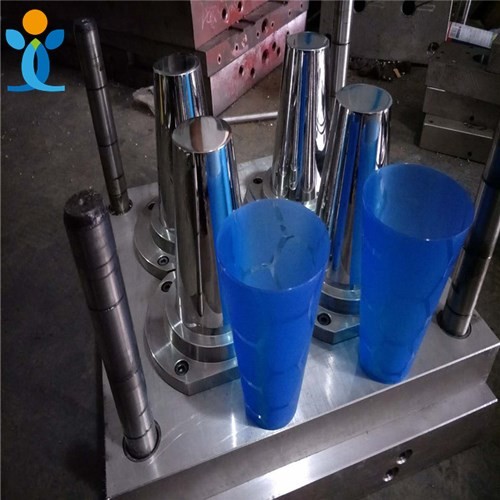
Produce 4 cups per shot — This 1x4 (four-cavity) injection mold is engineered for high-volume manufacturing of thin-walled plastic cups (drinking cups, dessert cups, portion cups), with four tall, highly polished, tapered core pins forming the internal cup shape.
Built with 718H, S136, or NAK80 polished steel on an LKM standard or custom mold base, it is designed for food-grade PP, PE, or PS thin-wall grades, offering corrosion resistance, mirror gloss, and long mold life for demanding food & beverage applications.
A hot runner valve gate system with a bottom direct/pin-point gate optimizes thin-wall flow and cycle time, while ISO 9001:2015, SGS and FDA (food contact) certified processes ensure consistent, hygienic quality.
Technical Specifications
Core Characteristics
High Efficiency (1x4)
Produces four cups per injection cycle, maximizing output for high-volume disposable products.
Tapered Core Design
The tapered cores allow easy demolding of deep, thin-walled parts without deformation.
High-Gloss Finish
Cores are polished to a mirror finish to keep the internal surface of the cup smooth and hygienic.
Fast Cycle Times
Optimized cooling and ejection systems enable rapid production, essential for low-cost disposable items.
Processing Difficulties & Countermeasures
1. Thin-Wall Filling & Short Shots
DifficultyCups are typically thin-walled (0.5-1.0 mm). Plastic must flow quickly and evenly to fill the tall, narrow cavity before it freezes off, or short shots occur.
CountermeasureHigh-speed injection with a hot runner valve gate system for rapid, balanced filling. Mold Flow Analysis (MFA) optimizes gate location and runner diameter for thin-wall flow.
2. Deep Core Cooling & Warpage
DifficultyThe tall, tapered cores are difficult to cool uniformly. Uneven cooling warps the cup, causing instability or stackability issues.
CountermeasureBaffled cooling channels or bubblers inside the tall cores bring coolant close to the surface. MFA optimizes cooling time and uniform temperature distribution.
3. Demolding of Deep, Thin-Walled Cups
DifficultyDeep, thin-walled cups can crack or deform during ejection if force is not evenly distributed.
CountermeasureStripper plates or sleeve ejectors push the cup evenly off the core. Air-assisted ejection breaks the vacuum for smooth release.
4. Core Alignment & Wear
DifficultyTall, slender cores are prone to misalignment or wear under high injection pressure, causing uneven wall thickness.
CountermeasureHigh-strength guide pins and bushings ensure precise alignment. Cores use hardened S136 or NAK80 steel to resist wear, with regular maintenance and alignment checks.
5. Gate Vestige & Bottom Quality
DifficultyThe bottom gate can leave a visible vestige or flow marks that affect appearance or function.
CountermeasureA pinpoint gate or hot runner valve gate at the bottom center, with optimized gate size to minimize vestige and a polished bottom surface.
6. Material Selection for Food Contact
DifficultyCups for food and beverages must meet strict hygiene standards; mold material must not corrode or release harmful substances.
CountermeasureFood-grade, corrosion-resistant steel (S136 or NAK80) on all plastic-contact surfaces, FDA-compliant certification, and thorough cleaning before delivery.
Applicable Industries
Our Workflow
A transparent, step-by-step process from design to delivery.
Stage 1: R&D Support & DFM Analysis
We support customer R&D for thin-walled food containers, creating or improving 3D files (UG, SolidWorks, ProE, AutoCAD, etc.), and provide a Mold Flow Analysis (MFA) report to optimize filling and cooling for thin-walled cups.
Stage 2: Mold Process & Hot Runner Integration
Mold design (DFM report) → check/approve → approved → make mold → integrate hot runner system → produce sample → sample confirmed → check final mold quality ready to export.
We specifically validate the cooling efficiency of the tall cores and the ejection system during this stage.
Stage 3: Sample Modification & Wall Thickness Optimization
If the first sample doesn't meet requirements (e.g., uneven wall thickness or warpage), we modify the mold and fine-tune the cooling circuits and injection parameters to meet your exact requirements.
Stage 4: Sample Delivery
Produce the customer's requested quantity (typically 500-1000 shots for validation), with free shipping.
Stage 5: Final Delivery
Deliver goods by sea or air; we can accommodate special requirements (like food-grade packaging or custom crating) based on customer needs.
Why Choose Us?
Partner with a trusted leader in precision injection molding.
20+ Years of Experience
More than 1,500 new injection molds and parts produced since 2006, with deep expertise in thin-wall molds and food-grade packaging for the food and beverage industry.
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification for peace of mind. Every mold base and steel insert meets rigorous dimensional and hygiene standards.
One-Stop Service
Value-added operations simplify your supply chain from design to delivery. From Mold Flow Analysis to food-grade certification, we handle the technical complexity so you don't have to.