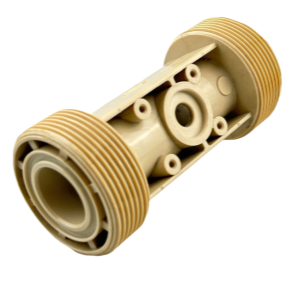
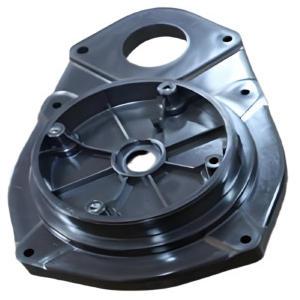
4 Cavities Injection Molding PEI Part
High-Performance Engineering Plastic – Polyetherimide (PEI)
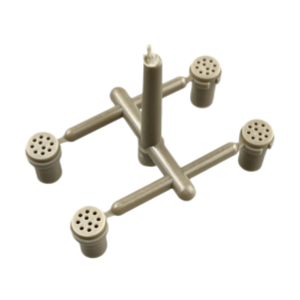
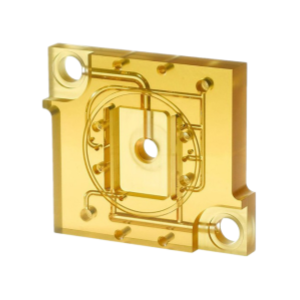
PEI (Polyetherimide) is a high-performance engineering plastic offering excellent heat resistance, high mechanical strength, and superior electrical insulation. It is widely used in automotive, electronics, aerospace, and medical applications. If you have such PEI parts or projects, Yixing Technology is your best choice.
Technical Specifications
| Parameter | Specification / Description |
|---|---|
| Material | PEI (Polyetherimide) – ULTEM™ 1000 Resin (Unreinforced / Natural Grade) |
| Color | Natural / Transparent Amber (Standard) / Customizable (Opaque & Transparent variants available) |
| Mold Cavity | 4 (1×4 balanced layout) – Multi-cavity mold designed for high-volume production |
| Mold Life | 500,000 cycles – Total output capacity of 2,000,000 parts (4 parts per cycle) |
| Tolerance | ±0.02mm (for critical dimensions, e.g., center bore & mounting holes) |
| Continuous Use Temp | Up to 170°C (RTI) / Glass Transition (Tg) at 217°C / HDT at 201–210°C |
| Shrinkage Rate | 0.5–0.7% (Flow Direction, Unfilled PEI) |
| Surface Finish | SPI-A1 Mirror Finish (Optical/Transparent areas) / SPI-B1 or Texture (External ribs & structural surfaces) |
| Lead Time |
Samples: 20–25 days Mass Production: 30–45 days (PEI requires high mold temps & slow cooling) |
| Processing | Injection Molding (Requires high mold temperature 135–165°C; Melt temp 350–400°C) |
| Application | Medical device component / Analytical instrument housing / Aerospace connector / Electrical insulation / Sterilizable trays |
| Packing | Anti-static bag + EPE foam + Export carton |
How We Mold the Multi-Cavity PEI Part?
1Thorough Drying
PEI is highly hygroscopic, so before molding, we need to dry it at 150°C for at least 4 hours to get moisture content below 0.02%. If we skip this or cut corners, we'll almost get the silver streaks or bubbles.
2Injection Process Control
Melt temperature should be set between 350°C and 400°C, with mold temperature maintained at 135°C–165°C to ensure proper flow and minimize internal stresses. For this 1-out-4 configuration, a balanced runner layout is essential, with all cavities arranged at equal distance from the sprue to ensure uniform filling. A hot runner system with a valve gate is recommended for the 1-out-4 layout, allowing independent temperature control at each nozzle and minimizing material waste. To match the symmetrical part layout, a circular cooling circuit is recommended, with baffles positioned around the core pins and inserts to ensure uniform cooling across all four cavities. Injection pressure generally ranges from 80–120 MPa, while holding pressure is about 50–70% of the injection pressure to reduce shrinkage and warpage. Injection speed should be medium to high to avoid premature freezing in the thin-walled sections, and back pressure is kept low at 0.3–0.7 MPa. Cooling time usually ranges from 20 seconds depending on wall thickness, and screw speed is set at 40–70 rpm.
3Stress Relieve
Post-mold annealing at 180°C–200°C for 2–4 hours is typically applied to relieve internal stress and optimize mechanical properties.
Multi-Cavity Cost Analyses
| Comparison Item | 1-Cavity Mold (1×1) | 1×4 Multi-Cavity Mold |
|---|---|---|
| Mold Cost | Lower upfront tooling cost; simpler mold base and runner system | Higher upfront tooling cost; requires balanced runner, additional cooling circuits, and tighter mold manufacturing |
| Cost per Part | Higher unit cost due to longer cycle time per part and higher machine time per piece | Lower unit cost at volume; cost amortized across 4 parts per cycle |
| Cycle Time | Same cycle time as multi-cavity, but only 1 part produced per cycle | Similar cycle time per shot, but 4 parts produced per cycle — up to 4× productivity |
| Production Capacity | Limited; suitable for low-to-medium volume or prototyping | High; ideal for mass production (e.g., 500,000 cycles → 2,000,000 parts) |
| Tolerance Capability | ±0.02 mm achievable with stable process | ±0.02 mm achievable, but tighter process control needed across all 4 cavities |
| MOQ Suitability | 100 – 1,000 pcs | 5,000 – 10,000 pcs or higher |
| Lead Time (Tooling) | Shorter mold manufacturing lead time | Longer mold manufacturing lead time due to complexity |
| Best Application | Prototyping, low-volume, complex geometry validation | High-volume production, stable part design, cost-sensitive mass manufacturing |
Our Workflow
A transparent, step-by-step process from design to delivery, tailored for 1×4 multi-cavity PEI part production.
Stage 1: R&D Support
We support customer R&D for PEI parts. Create the files or improve the design if needed (UG, SolidWorks, ProE, AutoCAD etc.), with early consideration for 1×4 mold layout, balanced runner, and uniform cooling.
Stage 2: Mold Process
Mold design (DFM report with 1×4 cavity layout, runner balance, and cooling circuit analysis) → check/approve → approved → make mold → produce sample → sample confirmed → check final mold quality ready to export.
Stage 3: Sample Modification
If the first sample does not satisfy the customer, we can modify the mold to meet customers' requirements, including cavity-to-cavity consistency and dimensional tolerance adjustments across all 4 cavities.
Stage 4: Sample Delivery
Produce the customer's requested quantity, free shipping.
Stage 5: Final Delivery
Deliver goods by sea or by air; special requirements can be accommodated based on customer demands.
Why Choose Our Custom PEI Parts?
Partner with a trusted specialist in high-performance PEI injection molding.
20+ Years Experience
Over 1,500 precision injection molds and parts successfully produced since 2006.
1×4 Multi-Cavity Tooling Expertise
Balanced runner and uniform cooling design ensure consistent quality across all 4 cavities, delivering up to 4× productivity with mold life rated at 500,000 cycles (2,000,000 parts total).
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification for your peace of mind.
One Stop Service
More value-added operations provided to simplify your supply chain from design to delivery.
Start Your Quote Here
CATEGORIES
LATEST NEWS
CONTACT US
- Mobile: +8615000908770
- Tel: +86-21-51662821
- WhatsApp: 8615000908770
- Email: contact@yxplasticmolding.com
- Address: Room 323, Building B, Hongchun Business Park, No. 980 Qinghewan Road, Qingpu District, Shanghai