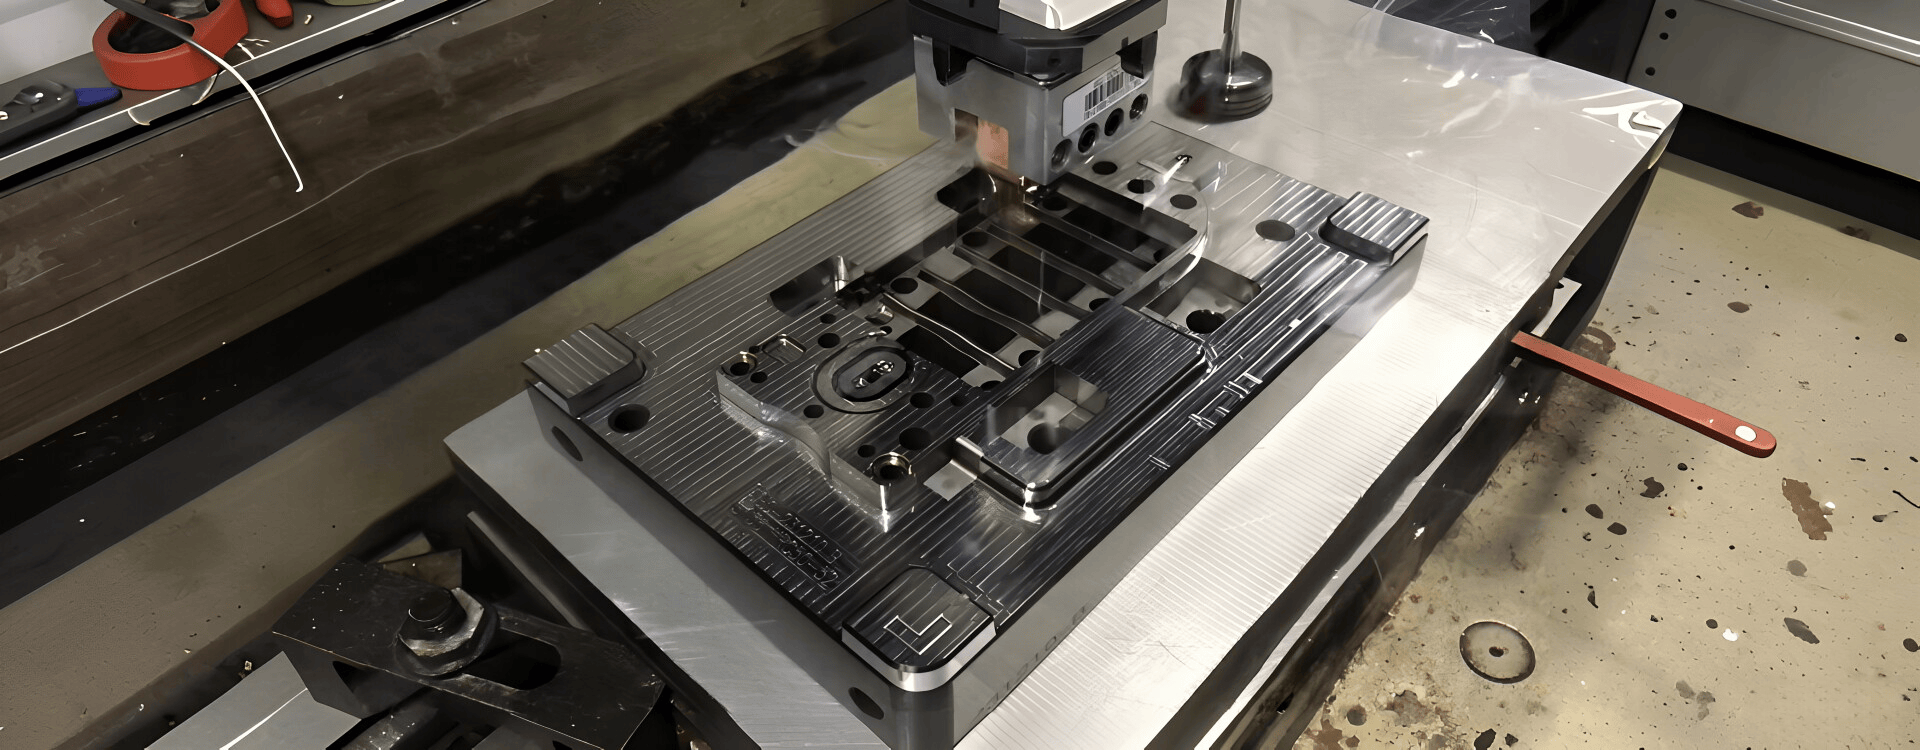
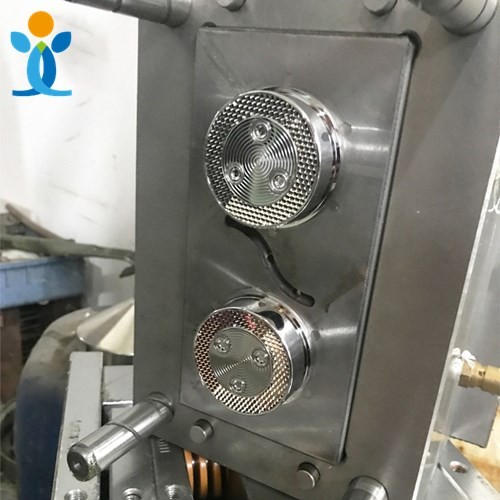
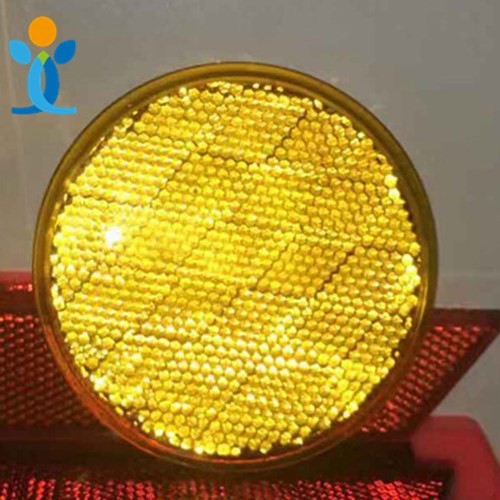
Produce 2 light components in 1 cycle — This 1x2 family mold produces plastic automotive lighting components such as headlight lenses, taillight housings, or reflector units, cutting machine time and labor costs for the customer.
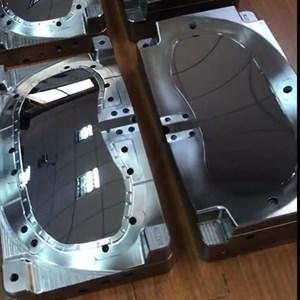
As seen in the image, the mold features two cavities of different sizes, both with high-precision textured surfaces to diffuse or direct light. Built with corrosion-resistant S136 steel and an LKM mold base, it is engineered for PC and PMMA optical-grade resins.
ISO 9001:2015 certified manufacturing and Mold Flow Analysis ensure balanced filling across both cavities, flawless optical finish and long mold life of 500,000+ shots.
Technical Specifications
Core Characteristics
High-Precision Optical Texture
The cavities feature fine, intricate textures (like concentric rings and micro-patterns) that are critical for light diffusion and aesthetics.
Family Mold Efficiency
Produces two different-sized light components in a single cycle, reducing machine time and labor costs for the customer.
Premium Surface Finish
Highly polished steel and precise texture etching ensure a flawless, transparent or highly reflective finish on the final part.
Durable Construction
Built to withstand the high injection pressures and temperatures required for engineering plastics like PC or PMMA.
Processing Difficulties & Countermeasures
1. Precision Texture Etching & Uniformity
DIFFICULTYThe fine concentric rings and micro-patterns must be perfectly replicated on both cavities. Any inconsistency in texture depth or pattern causes uneven light diffusion or visible cosmetic defects.
SOLUTIONHigh-precision CNC and EDM create the base geometry, followed by chemical etching or laser engraving for the texture. Strict quality control with 3D microscopy ensures the texture is identical across both cavities.
2. Optical Surface Polishing (No Flow Marks)
DIFFICULTYFor transparent or highly reflective parts, flow marks, weld lines, or polishing scratches are unacceptable. The steel must be polished to a mirror finish (SPI A1-A2) before texturing.
SOLUTIONDiamond paste polishing and ultrasonic polishing achieve a flawless mirror surface. Gate location and injection speed are optimized to eliminate weld lines and flow marks during molding.
3. Family Mold Balancing
DIFFICULTYThe two cavities need balance correctly.
SOLUTIONMold Flow Analysis (MFA) simulates the filling of both cavities; runner diameters and gate sizes are then tuned specifically for each cavity to ensure simultaneous, balanced filling.
4. Warpage & Shrinkage Control
DIFFICULTYAutomotive light parts have complex geometries and tight dimensional tolerances. PC and PMMA shrink differently, and uneven cooling can cause warpage.
SOLUTIONConformal or baffled cooling channels ensure uniform temperature across curved surfaces. Holding pressure and cooling time are optimized during sampling to minimize internal stress and warpage.
5. Ejection of Fragile Optical Parts
DIFFICULTYCar light lenses can be thin and fragile. Standard ejector pins can leave marks or crack the part during ejection.
SOLUTIONLarge-diameter sleeve ejectors or air-assisted ejection distribute the force evenly, and the ejection stroke is carefully calibrated to prevent deformation.
Applicable Industries
- Automotive Lighting: Headlight lenses, taillight covers, fog light housings, turn signal lenses.
- Automotive Interiors: Decorative light covers, instrument panel light guides.
- General Lighting: High-end outdoor LED lighting covers (if the material matches).
Our Workflow
A transparent, step-by-step process from design to delivery.
R&D Support & DFM Analysis
We support customer R&D for automotive lighting components, creating or improving 3D files (UG, SolidWorks, ProE, AutoCAD, etc.). Crucially, we provide a Mold Flow Analysis (MFA) report to balance filling across the two cavities and predict potential warpage.
Mold Process & Texture Integration
Mold design (DFM report) → check/approve → approved → make mold → integrate texture etching → produce sample → sample confirmed → check final mold quality ready to export.
We specifically validate the optical clarity and texture uniformity of both cavities during this stage.
Sample Modification & Optical Optimization
If the first sample doesn't meet requirements (e.g., flow marks, warpage, or texture inconsistency), we modify the mold, fine-tuning the gate sizes, cooling circuits and injection parameters to meet your exact optical requirements.
Sample Delivery
Produce the customer's requested quantity (typically 500-1000 shots for validation), with free shipping.
Final Delivery
Deliver goods by sea or air; we can accommodate special requirements (like custom crating for the heavy mold) based on customer needs.
Why Choose Us?
Partner with a trusted leader in precision injection molding.
20+ Years of Experience
We have produced more than 1,500 new injection molds and parts since 2006, with deep expertise in family molds and optical-grade molds for the automotive lighting industry.
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification. Every mold base, steel insert and textured surface meets rigorous dimensional and optical standards.
One-Stop Service
More value-added operations simplify your supply chain from design to delivery. From Mold Flow Analysis to texture etching and optical polishing, we handle the complexity for you.