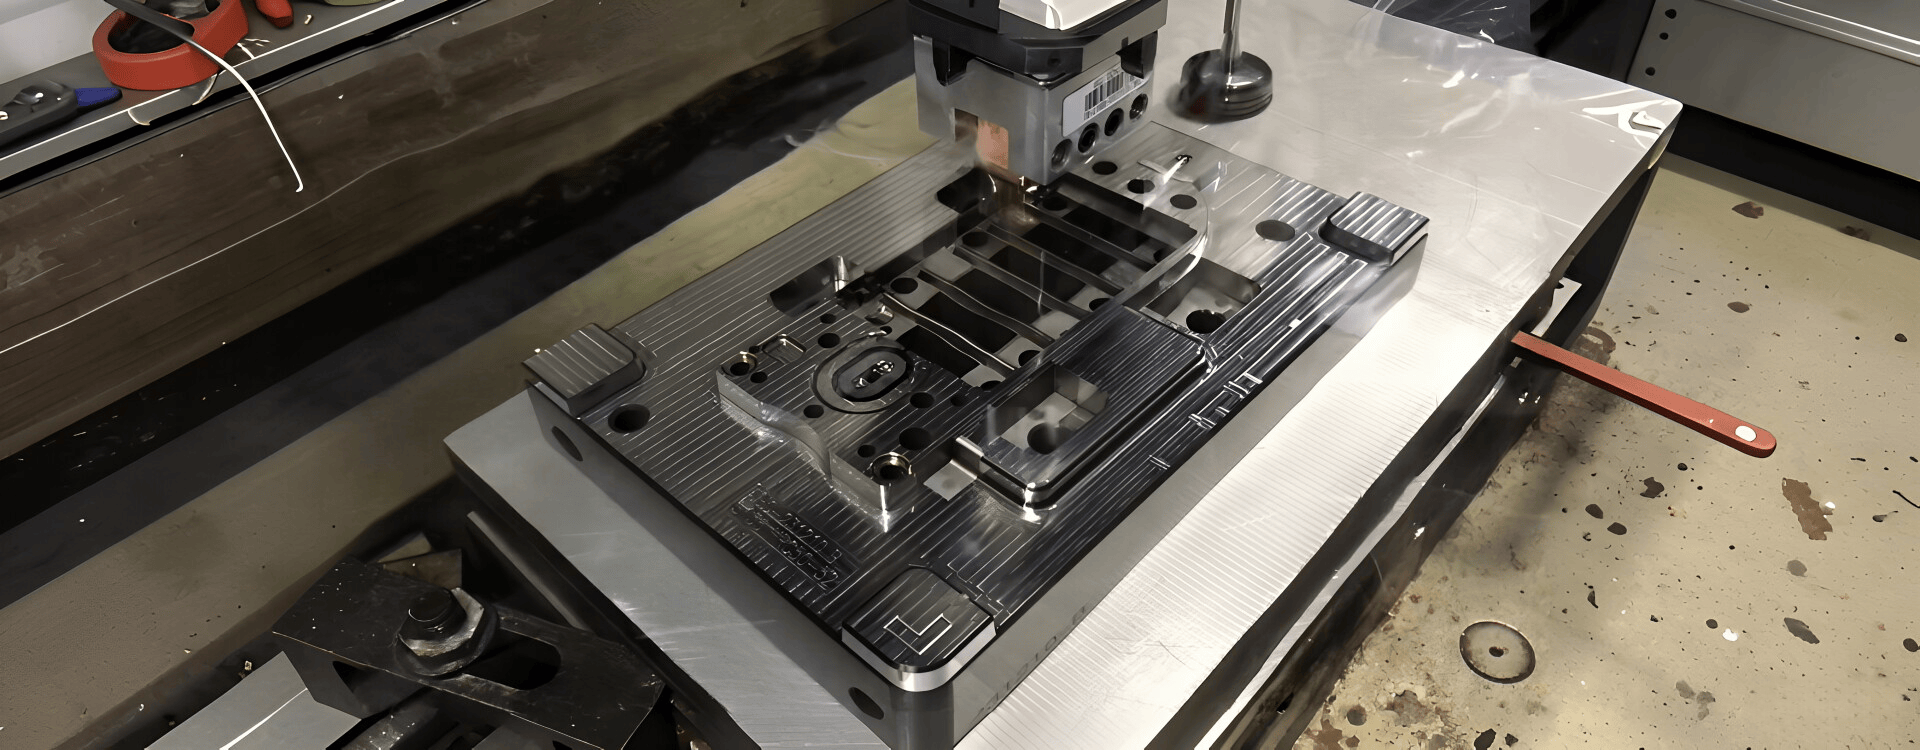
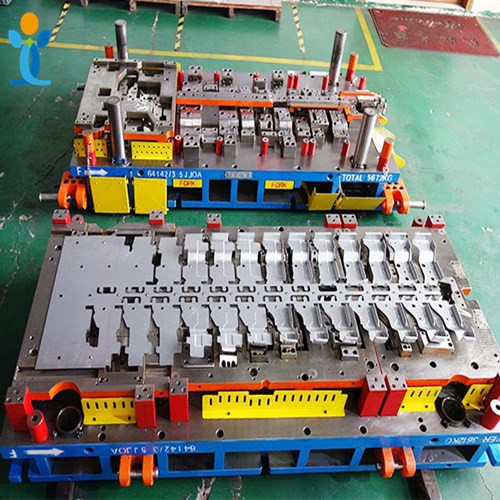
This multi-station progressive die mass-produces metal supports — such as structural brackets, mounting supports, or chassis reinforcement plates. Each press stroke advances the metal strip through a series of distinct stations, so a finished support is produced with every stroke at high speed.
Built with DC53 tool steel for long life and wear resistance, the die is rated for approximately 1,000,000 strokes. It runs on an 800 kN press and is equipped with automatic feeding and take-up systems, forming 1.0 mm thick SPCC / SGCC or stainless steel strip at tolerances down to ±0.05 mm.
Technical Specifications
Key Features of This Mold
1. Multi-Station Layout (Progressive Design)
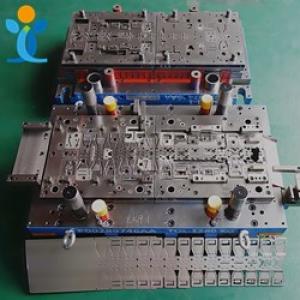
The die block contains multiple distinct stations. Each station performs a specific operation (e.g., piercing, notching, bending, forming), and the part moves forward one station with each press stroke.
2. Heavy-Duty Guide System
Four large, prominent guide pillars with helical springs maintain perfect alignment between the upper and lower die halves during high-speed stamping, ensuring precise support formation.
3. Complex Inserts and Blocks
The lower die contains numerous segmented blocks and inserts. This modular design eases maintenance — if one bending or cutting section wears out, you replace only that insert, not the entire die block.
4. High-quality Base and Structure
The high quality steel base with lifting rings can withstand the significant tonnage and vibration of a mechanical press.
5. Integrated Spring & Stripper design
Smaller springs and stripper plates hold the metal strip flat during cutting and strip the finished part off the punches after forming, preventing the material from sticking to the upper die.
6. Side Cam Bending Mechanism
A cam-driven side bending unit (the angled block on the side of the lower die) allows complex bends that cannot be achieved with standard vertical press motion, forming the support's side walls or flanges.
Manufacturing Process
Progressive die stamping integrates multiple operations into a single die set. The process flow for a metal support usually follows this sequence.
1. Piercing
The first stations punch pilot holes and create internal cutouts or slots in the metal strip.
2. Blanking / Notching
The outer profile of the support is partially cut to prepare for forming.
3. Bending / Forming
Successive stations bend the material into the final support shape (e.g., creating the mounting tabs, reinforcement ribs, or U-channels).
4. Side Bending (Cam Operation)
A cam-driven station bends the side flanges or complex angles that require horizontal movement.
5. Trimming
Any excess material or connecting tabs are trimmed off to define the final outline.
6. Separation
The final station cuts the completed support from the carrier strip.
Challenges & Solutions
1. Dimensional Accuracy and Consistency
ChallengeMaintaining the precise shape and position of the support, especially during high-speed production, is difficult.
SolutionWe use high-precision guide pillars and bushings to ensure the upper and lower dies stay perfectly aligned. Regular inspection and maintenance of the cutting clearances are also critical.
2. Tool Wear and Life
ChallengeRepeated high-impact stamping can cause wear on the cutting edges and forming surfaces.
SolutionWe use high-quality tool steel DC53, which offers high wear resistance. A robust maintenance schedule, including proper lubrication with graphite-based oils, can extend die life by up to 30%.
3. Strip Feeding and Buckling
ChallengeFeeding the metal strip accurately through multiple stations without jamming or buckling is a common issue, especially with thicker material.
SolutionWe use a reliable automatic feeding system and ensure the strip is guided properly through the die. Maintaining balanced strip tension is key to preventing deformation.
4. Springback and Material Thickness Variance
ChallengeThe metal tends to spring back after bending, affecting final dimensions. Different material batches can also cause inconsistencies.
SolutionWe compensate for springback during the die design phase. For high-precision supports, we add a sizing station to correct the shape after forming, and run regular quality checks of incoming raw material.
5. Cam Bending Accuracy
ChallengeThe side cam bending mechanism is prone to wear and alignment issues, affecting the angle and position of the side flanges.
SolutionWe use high-strength cam drivers and wear plates, regularly inspect the cam contact surfaces, and adjust the cam stroke to maintain consistent bend angles.
Application Scenarios of Progressive Dies
Why These Industries Use Progressive Dies
High Volume
Produces thousands of parts per hour for demanding mass-production schedules.
High Precision
Ideal for tight-tolerance electronic and automotive parts held within ±0.05 mm.
Cost-Effective
Low unit cost for mass production thanks to integrated, single-die-set processing.
Automation
Runs continuously with automatic feeding and take-up for minimal manual handling.
Our Process
Inquiry → DFM Analysis → Die Design → Die Manufacturing → Sample Approval → Small Batch Order → Mass Production → Shipping.
1. Inquiry
Customer provides part drawings, material specs, tolerance requirements, and annual volume for the metal support.
2. DFM Analysis (Design for Manufacturing)
Our Engineers analyze strip layout, material utilization, bending sequence, and potential forming defects before make the final mold drawing— and send feedback to the customer to optimize the design.
3. Die Design
3D CAD design of the progressive die, including strip layout and station arrangement, punch and die block design, guide pillar and spring system, stripper plate and ejection mechanism, and the cam bending mechanism design.
4. Die Manufacturing
Material procurement (DC53, SKD11, D2, etc.), CNC machining, wire EDM and grinding, heat treatment for punches and inserts, and assembly and fitting of the upper and lower die halves.
5. Sample Approval
Trial run on the press. First articles are measured and inspected, and we send samples to the customer for dimensional and functional approval.
6. Small Batch Order
After sample approval, we run a small production batch to verify die stability, consistency, and production speed.
7. Mass Production
Full-scale production begins. The progressive die runs continuously with automatic feeding, producing thousands of metal supports per hour.
8. Shipping
We pack, label, and ship finished supports to the customer on schedule.
Why Choose Us for Progressive Die Solutions?
Partner with a trusted leader in precision progressive die manufacturing.
20+ Years of Experience
We have successfully produced more than 1,500 progressive dies and stamped parts since 2006.
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification for your peace of mind.
One-Stop Service
More value-added operations provided to simplify your supply chain from design to delivery.
In-House Die Manufacturing
Complete capability from DFM analysis and die design to machining, assembly, and trial runs — all under one roof.
High-Speed Production
Progressive dies designed for automatic feeding and continuous stamping, producing thousands of precision metal supports per hour.