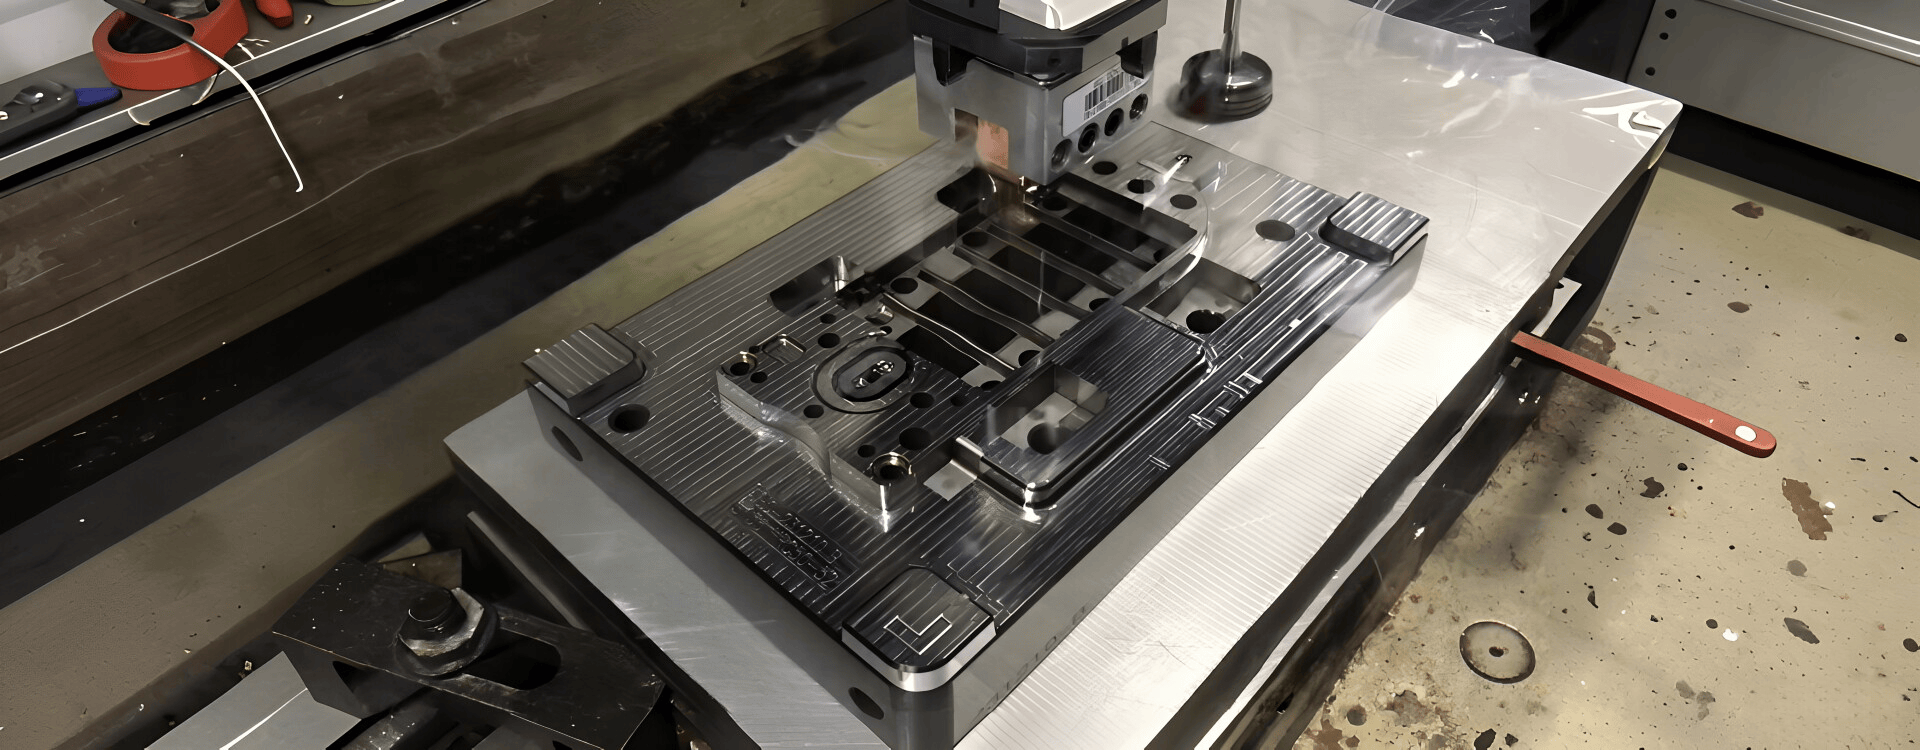

A massive 1x1 single-cavity mold for heavy-duty pallets — This injection mold is designed specifically to produce large, load-bearing plastic pallets. It features a massive core and cavity set with a complex ribbed structure that forms the pallet's load-bearing grid and feet.
Built on a custom heavy-duty steel base with pre-hardened P20 / 718H / 2738 steel for the core and cavity, the mold is engineered for PP / HDPE materials, delivering the strength, rigidity and dimensional stability demanded by large-part industrial molding.
ISO 9001:2015 certified manufacturing ensures consistent quality and a mold life of 500,000+ shots. A cold runner system (with an optional hot runner valve-gate upgrade for large parts) is paired with Mold Flow Analysis (MFA) to balance filling, control shrinkage and minimize warpage.
Technical Specifications
Core Characteristics
1. Massive Scale & High Tonnage
Capable of producing standard-sized pallets (e.g., 1200x1000mm or 1100x1100mm) with high structural integrity.
2. Optimized Rib Design
The complex grid pattern on the core side ensures maximum load capacity while minimizing material usage and weight.
3. Deep Core & Cooling
The deep core design requires specialized cooling and ejection systems to handle the large part volume and thick walls.
4. High Durability
Built with high-strength steel to withstand the immense injection pressures and clamping forces required for large-part molding.
Processing Difficulties & Countermeasures
1. Extreme Mold Weight & Handling
DifficultyA large-part mold of this size (about 8 tons) requires specialized cranes, heavy-duty clamping systems, and precise alignment during assembly and installation. Lifting rings on the mold plates confirm its massive weight.
CountermeasureWe design the mold with reinforced lifting rings and heavy-duty guide pins. We also provide a detailed installation and handling manual and can assist with on-site setup if required.
2. Deep Core & Uniform Cooling
DifficultyThe deep core (the grid structure) creates a large volume of plastic that must cool uniformly. If cooling is uneven, the pallet will warp, making it unstable for stacking.
CountermeasureWe design conformal cooling channels or baffled cooling systems deep inside the core. We also use Mold Flow Analysis (MFA) to simulate the cooling process and optimize the cooling-circuit layout.
3. High Injection Pressure & Clamping Force
DifficultyFilling a large, thin-walled plastic pallet requires extremely high injection pressure and clamping force (1,500 tons). Any weakness in the mold structure can lead to flashing or mold deformation.
CountermeasureWe use high-strength 718H or 2738 steel for the core and cavity. The mold base uses thick support plates and reinforced ribs to withstand the pressure. We also recommend a high-tonnage injection machine with precise pressure control.
4. Ejection of Large, Flexible Parts
DifficultyThe plastic pallet is large and flexible. Ejecting it without deformation or cracking requires a carefully balanced ejection system with many ejector pins or a stripper plate.
CountermeasureWe design a balanced ejector pin layout with large-diameter pins distributed evenly across the pallet's grid structure. We also use air-assisted ejection to help release the part from the deep core.
5. Warpage & Dimensional Stability
DifficultyPP and HDPE have high shrinkage rates. The pallet's large, flat surface is prone to warping, which can affect stackability and load-bearing capacity.
CountermeasureWe optimize the holding pressure and cooling time during sampling. We also design the mold with adjustable cooling zones to fine-tune the temperature distribution and minimize warpage.
6. Gate Vestige & Flow Marks
DifficultyThe gate location must be carefully chosen to ensure balanced filling and avoid visible flow marks on the pallet's surface.
CountermeasureWe use Mold Flow Analysis to determine the optimal gate location. For large pallets, we often recommend a hot runner valve gate system to eliminate cold runner waste and ensure a clean gate vestige.
Applicable Industries
Our Workflow
A transparent, step-by-step process from design to delivery.
R&D Support & DFM Analysis
We support customer R&D for large industrial pallets. We create or improve 3D files (UG, SolidWorks, ProE, AutoCAD, etc.). Crucially, we provide a Mold Flow Analysis (MFA) report to optimize the rib structure, gate location, and cooling layout.
Mold Process & Heavy-Duty Integration
Mold design (DFM report) → check/approve → approved → make mold → integrate hot runner system → produce sample → sample confirmed → check final mold quality ready to export.
We specifically validate the structural integrity and cooling efficiency of the deep core during this stage.
Sample Modification & Warpage Optimization
If the first sample doesn't meet the customer's requirements (e.g., warpage or dimensional issues), we can modify the mold. We fine-tune the cooling circuits and holding pressure to meet your exact requirements.
Sample Delivery
Produce the customer's requested quantity (typically 50-100 shots for validation due to the large part size), with free shipping.
Final Delivery
Deliver goods by sea or air; we can accommodate special requirements (like custom heavy-duty crating for the 8+ ton mold) based on customer needs.
Why Choose Us?
Partner with a trusted leader in precision injection molding.
20+ Years of Experience
We have successfully produced more than 1500 new injection molds and parts since 2006. We have deep expertise in large-scale molds and heavy-duty industrial parts for the logistics and warehousing industries.
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification for your peace of mind. We ensure every mold base and steel insert meets rigorous dimensional and structural standards.
One-Stop Service
We provide more value-added operations to simplify your supply chain from design to delivery. From Mold Flow Analysis to heavy-duty machine matching (1500+ tons), we handle the technical complexity so you don't have to.