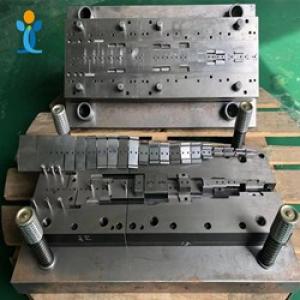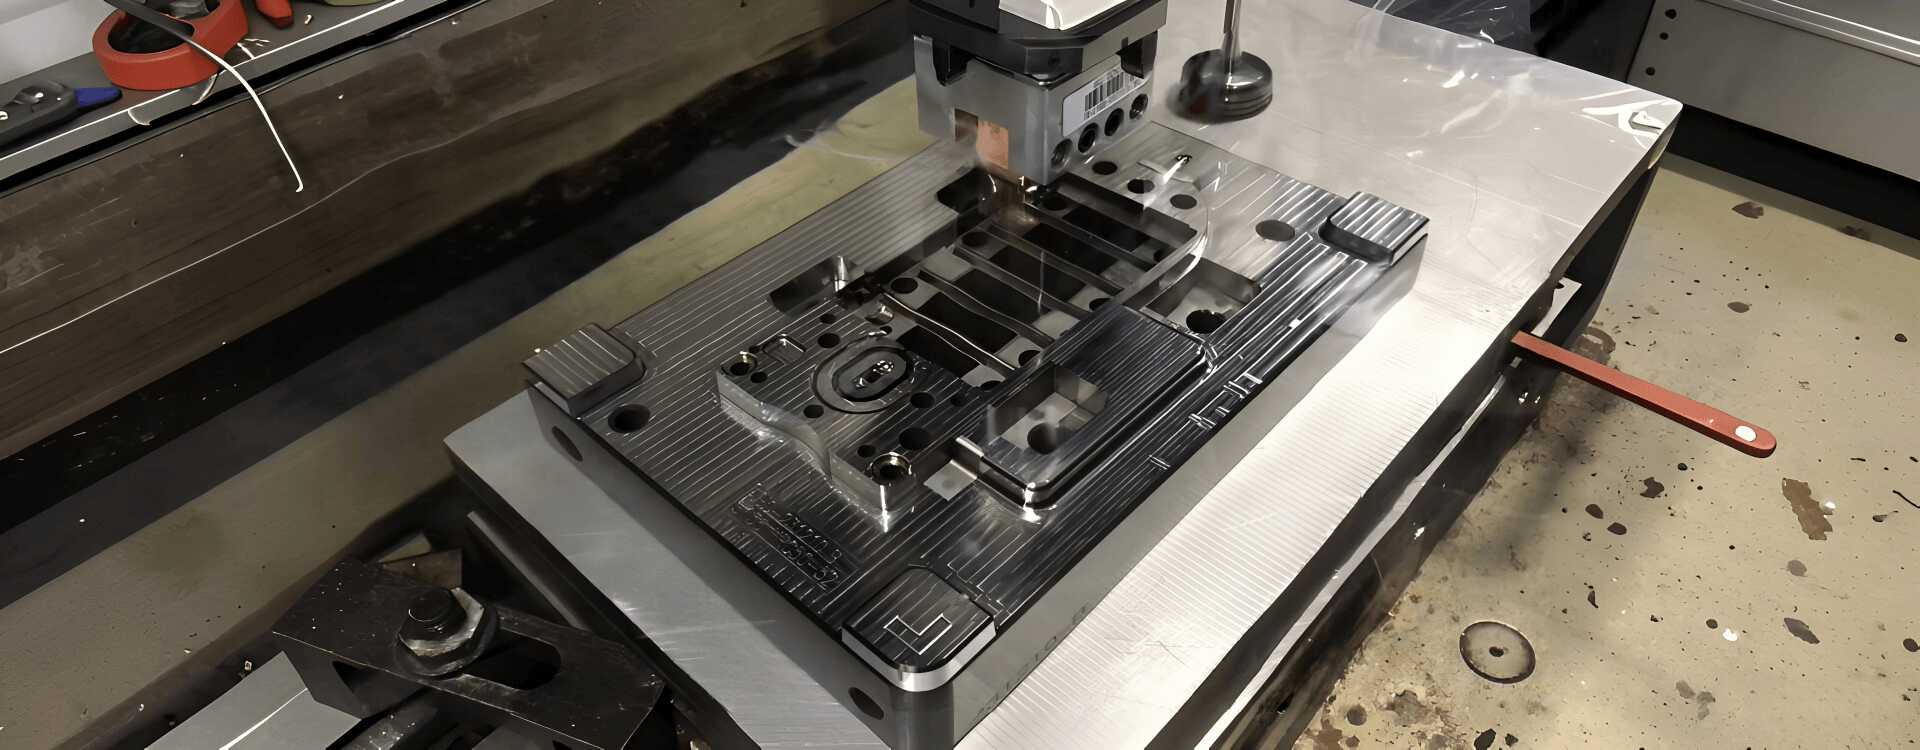


2-in-1 family mold: two parts, one cycle — This mold produces two different plastic components in a single injection cycle. As seen in the image, it utilizes a cold runner system with edge gates, making it a cost-effective solution for producing paired parts (e.g., a cap and its base, or two distinct components for an assembly).
Built on a standard LKM mold base with 718 steel, the mold is designed for HDPE processing, offering stable performance and long service life for pipe fitting and daily chemical components.
ISO 9001:2015 certified manufacturing process ensures consistent quality. The cold runner + edge gate layout is straightforward to maintain, clean, and troubleshoot, and Mold Flow Analysis is used to balance filling across the two cavities.
Technical Specifications
Core Characteristics of This 2-in-1 Family Plastic Mold
Cost-Effective Production
The 2-in-1 family mold design allows you to produce two different parts in one machine cycle, reducing machine time and labor costs.
Standard & Durable
Built on a standard LKM mold base with 718 steel, ensuring long-term stability and a mold life of over 500,000 shots.
Simple & Reliable
The cold runner + edge gate system is straightforward to maintain, clean, and troubleshoot, making it ideal for HDPE processing.
Compact Design
Weighing approximately 300 kg, it is optimized for standard 200-ton injection machines, minimizing the need for specialized equipment.
Processing Difficulties & Countermeasures
1Balancing the Two Different Cavities
In a family mold, two completely different parts (different shapes and wall thicknesses) must fill simultaneously. If one cavity fills faster, it can overpack one part and cause short shots in the other.
We use Mold Flow Analysis (MFA) to simulate the filling process. We then precisely adjust the runner dimensions and edge gate sizes for each cavity to ensure both parts fill at the same time under the same injection pressure.
2Warpage & Shrinkage Control (HDPE)
HDPE has a high shrinkage rate (1.5% - 3.0%), and the two different part geometries may warp differently upon cooling.
We design custom cooling circuits specific to each cavity's geometry. We also apply scientific injection molding principles during sampling to optimize holding pressure and cooling time, ensuring dimensional stability for both parts.
3Gate Vestige & Cosmetic Defects
The edge gate system can leave a visible gate mark on the side of the part, which may be unacceptable for certain cosmetic applications.
We position the edge gates on non-cosmetic surfaces or hidden areas of the part. We optimize the gate size to minimize the vestige, and we can polish the gate area to match the specified MT or YS surface finish.
4Ejection System Complexity
Since the two parts have different shapes, they may require different ejection forces. A single ejector plate must push both parts out without damaging either one.
We design a balanced ejector pin layout with different pin sizes and positions for each part. We also use sleeve ejectors or stripper plates where necessary to distribute the ejection force evenly and prevent white marks or deformation.
5Mold Maintenance & Alignment
The 2-in-1 family mold has more complex internal structures, and the cold runner system requires regular cleaning to prevent material buildup.
We use high-quality guide pins and bushings for precise alignment. The mold includes easy-access panels for quick cold-runner cleaning. We also provide a detailed maintenance manual with the mold delivery.
Our Workflow
A transparent, step-by-step process from design to delivery.
R&D Support & DFM Analysis
We support customer R&D for paired plastic components. We create or improve 3D files (UG, SolidWorks, ProE, AutoCAD, etc.). Crucially, we provide a Mold Flow Analysis (MFA) report to balance filling across the two cavities, ensuring both parts are produced without defects.
Mold Process & Cold Runner Integration
Mold design (DFM report) → check/approve → approved → make mold → integrate cold runner system → produce sample → sample confirmed → check final mold quality ready to export.
We specifically validate the edge gate placement and the cooling efficiency for both distinct product shapes during this stage.
Sample Modification & Gate Optimization
If the first sample doesn't meet the customer's requirements (e.g., flow marks or dimensional inconsistencies), we can modify the mold. We fine-tune the runner dimensions and gate sizes to ensure perfect filling for both parts.
Sample Delivery
Produce the customer's requested quantity (typically 500-1000 shots for validation), with free shipping.
Final Delivery
Deliver goods by sea or air; we can accommodate special requirements (like custom crating for the 300 kg mold) based on customer needs.
Why Choose Us?
Partner with a trusted leader in precision injection molding.
20+ Years of Experience
We have successfully produced more than 1500 new injection molds and parts since 2006. We have deep expertise in family molds and cold runner systems for the daily chemical and household goods industries.
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification for your peace of mind. We ensure every LKM mold base and 718 steel insert meets rigorous dimensional standards.
One-Stop Service
We provide more value-added operations to simplify your supply chain from design to delivery. From Mold Flow Analysis to 200-ton machine matching, we handle the technical complexity so you don't have to.