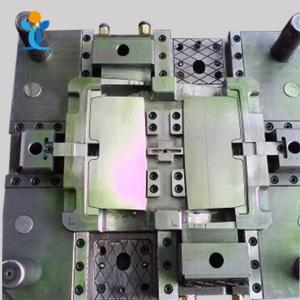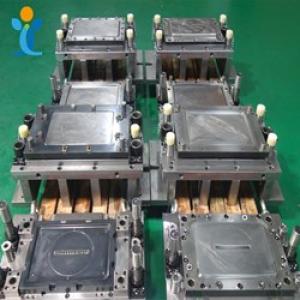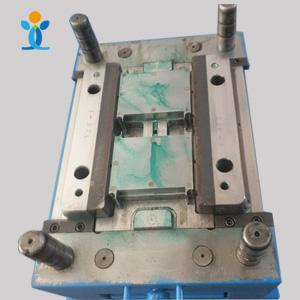
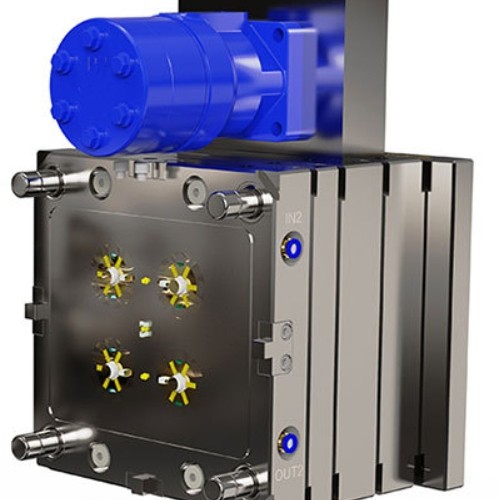
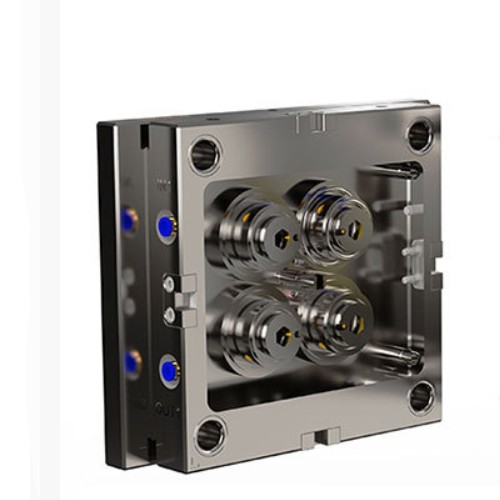
Produce 4 caps per shot with zero runner waste — This high-precision, multi-cavity injection mold is designed specifically to produce plastic caps and closures, valves, joints and connectors. Utilizing a 1x4 hot runner valve-gate system, it injects molten plastic directly into four cavities simultaneously, producing finished caps with no runner waste.
Built on a P20 pre-hardened steel mold base with S136 corrosion-resistant core and cavity steel, it is engineered for HDPE and rated for 500,000 to 1,000,000 cycles, delivering long mold life and consistent part quality.
The hot runner valve-gate system, custom drilled cooling channels and stripper/sleeve ejection combine to eliminate cold-runner scrap, shorten cycle time and leave a clean, minimal gate vestige — ensuring a high-quality, premium finish on every cap.
Technical Specifications
Core Characteristics
Zero Waste (Runnerless)
The hot runner system eliminates cold runner waste, saving raw material costs and eliminating the need for secondary trimming.
High Efficiency
1x4 cavity design with valve-gate technology enables faster cycle times and higher output compared to cold runner molds.
Superior Aesthetics
Valve-gate nozzles leave a clean, minimal gate vestige on the cap top, ensuring a high-quality, premium finish.
Precision & Consistency
Balanced hot runner manifold ensures each of the 4 caps has identical weight, dimensions and sealing performance.
Processing Difficulties & Countermeasures
1. Multi-Cavity Balance
DifficultyAchieving consistent filling and weight for each of the 4 cavities (a 1x4 layout) to avoid warpage or short shots.
CountermeasureUse Mold Flow Analysis (MFA) software to simulate and optimize the hot runner manifold's internal flow channels for balanced pressure and temperature distribution.
2. Valve Gate Precision
DifficultyThe hot runner nozzles (valve gates) require precise actuation and thermal control to prevent stringing, drooling, or gate vestige defects.
CountermeasureImplement a multi-zone temperature controller for each nozzle and a sequential valve gate system to control the opening/closing timing precisely.
3. Tight Tolerances for Cap Fit
DifficultyCaps require very tight tolerances on the internal thread or snap-fit features to ensure a proper seal on the bottle.
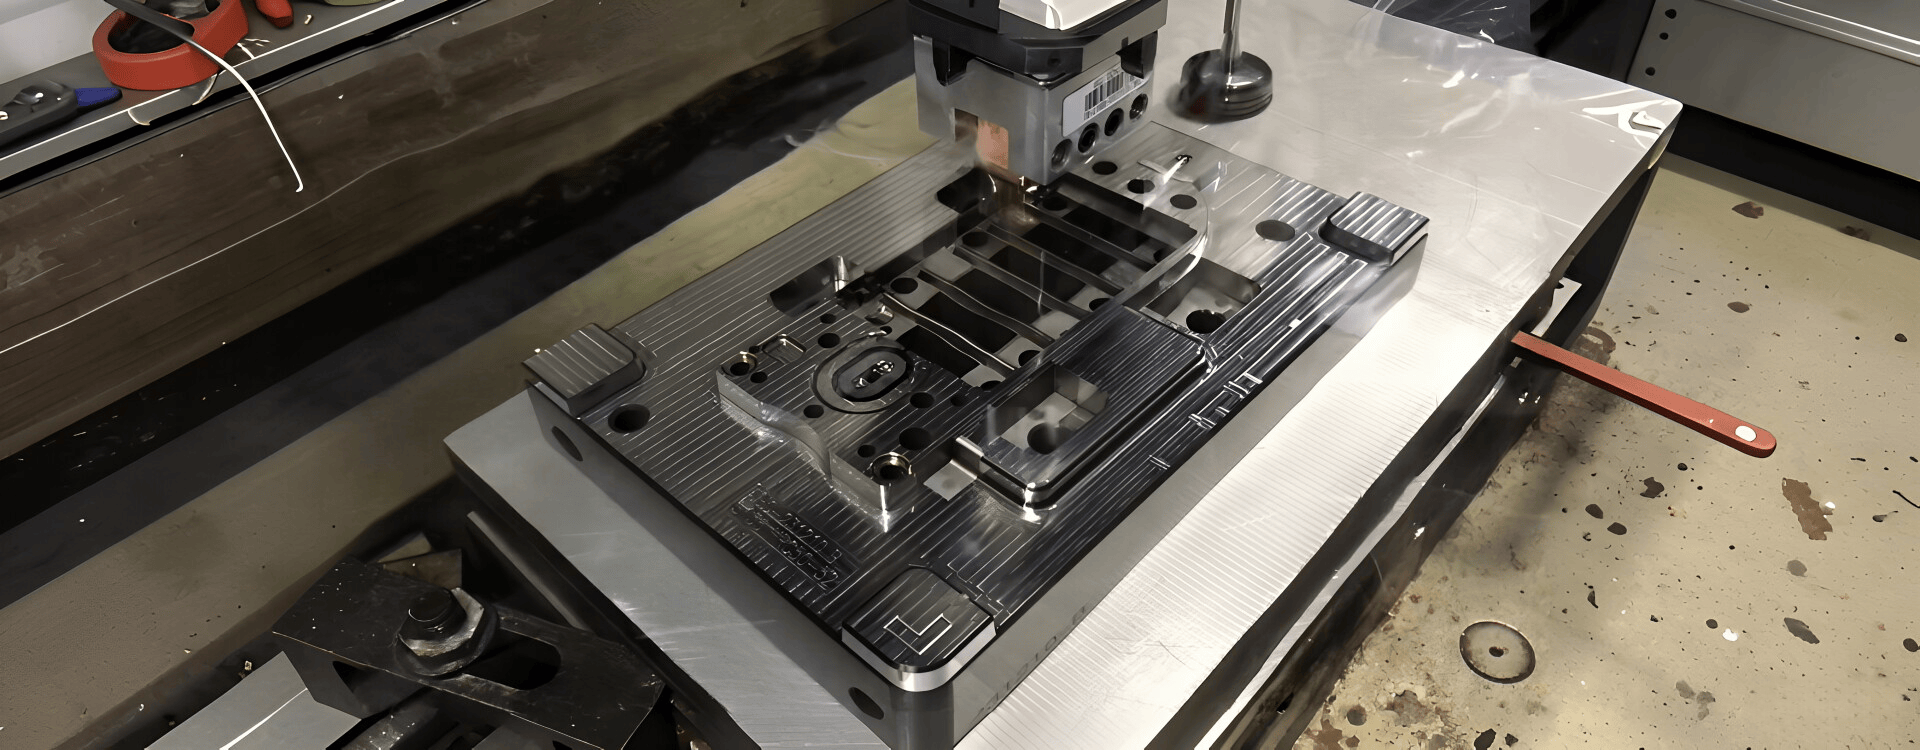
CountermeasureUse high-speed CNC machining for the core/cavity inserts and apply EDM (Electrical Discharge Machining) for sharp internal corners. Regular CMM inspection of the first shots is necessary.
4. Cooling Efficiency
DifficultyThick cap walls and the central core can lead to long cycle times due to slow cooling.
CountermeasureDesign conformal cooling channels (using 3D-printed inserts or baffles) to bring coolant closer to the part surface, and use a high-efficiency chiller to maintain a consistent mold temperature.
5. Thermal Expansion & Alignment
DifficultyThe manifold's heat can cause expansion, leading to misalignment between the hot runner nozzles and the mold gates.
CountermeasureDesign the manifold with a "floating" thermal expansion allowance and ensure the nozzles are aligned with the gate seals to prevent leakage.
6. Gate Vestige & Aesthetics
DifficultyVisible gate marks or "vestiges" on the top of the cap can be a cosmetic defect.
CountermeasureUse valve gate nozzles with a precise tip design to leave a minimal, flush gate mark. Optimize the exact gate position and geometry during the design phase.
Applicable Industries
Our Workflow
A transparent, step-by-step process from design to delivery.
Stage 1: R&D Support & DFM Analysis
We support customer R&D for high-precision caps. We create or improve 3D files (UG, SolidWorks, ProE, AutoCAD, etc.). Crucially, we provide a Mold Flow Analysis (MFA) report to optimize the 1x4 hot runner layout, ensuring balanced filling and minimal warpage before cutting steel.
Stage 2: Mold Process & Hot Runner Integration
Mold design (DFM report) → check/approve → approved → make mold → integrate hot runner system → produce sample → sample confirmed → check final mold quality, ready to export.
We validate the manifold's thermal balance and the precise actuation of the valve gates during this stage.
Stage 3: Sample Modification & Gate Optimization
If the first sample does not meet the customer's requirements (e.g., gate vestige issues or cap dimension tolerances), we can modify the mold. We fine-tune the valve gate timing and cooling circuits to meet your exact requirements.
Stage 4: Sample Delivery
Produce the customer's requested quantity (typically 500-1000 shots for validation), with free shipping.
Stage 5: Final Delivery
Deliver goods by sea or air; we can accommodate special requirements (like custom crating or specific logistics for the hot runner controller) based on customer needs.
Why Choose Us?
Partner with a trusted leader in precision injection molding.
20+ Years of Experience
We have successfully produced more than 1,500 new injection molds and parts since 2006. We have deep expertise in complex hot runner systems and multi-cavity cap molds.
ISO9001 Certificated
Strict quality control system, providing ROHS/CE certification for your peace of mind. We ensure every hot runner nozzle and valve gate pin meets rigorous dimensional and thermal standards.
One-Stop Service
We provide more value-added operations to simplify your supply chain from design to delivery. From Mold Flow Analysis to valve gate controller matching, we handle the technical complexity so you don't have to.